PROFESSIONAL CNC MACHINING SERVICES IN HOUSTON

Professional CNC Machining Solutions In Houston Since 1964

Founded in 1964, Lowrance Machine has supported manufacturers and industrial customers for more than 60 years. Its long history in the local area makes it a dependable partner for custom parts, repairs, and demanding production work.

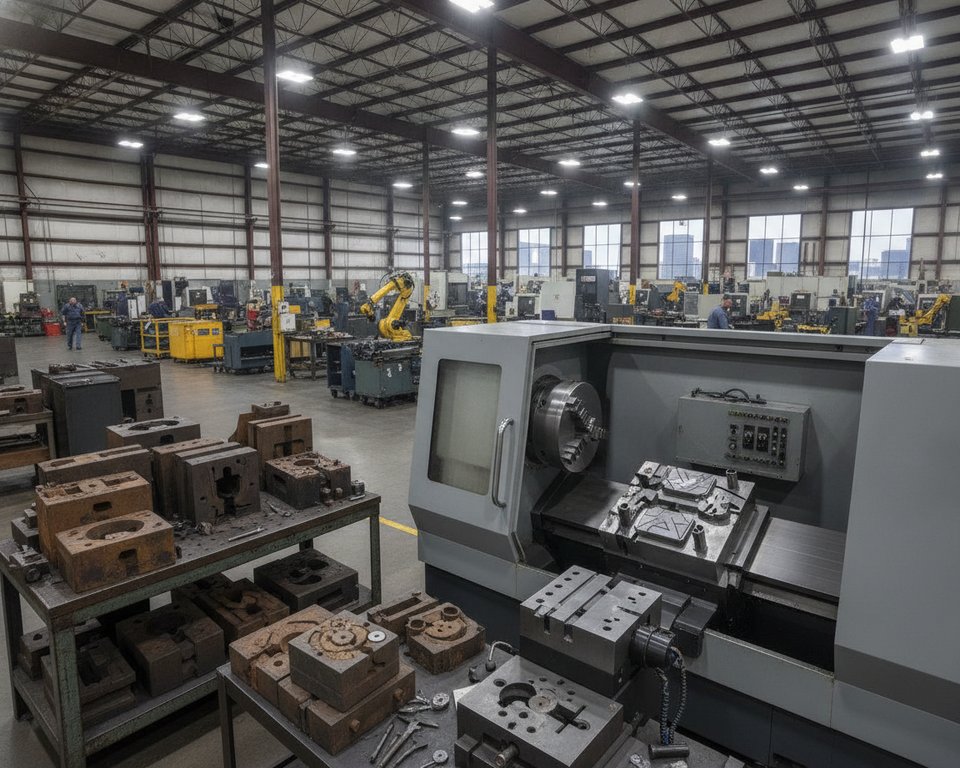
Modern CNC equipment is used alongside traditional manual methods, allowing the team to select an approach suited to each job. This combination accommodates production needs ranging from small runs and repairs to complex projects. Experience in manufacturing and other industries also helps the team develop practical solutions.


Available services include turning, milling, manual work, custom mold engineering, and industrial support. Customers have the opportunity to discuss precision needs and quality goals with the team ahead of the work.

To discuss a project, visit Lowrance Machine at 13510 East Hardy Road, Houston, TX 77039. Get in touch with the shop today to ask about a service or obtain a quote.

Professional CNC Machining Services In Houston For Complex Industrial Projects

More than one machining approach may be necessary for complex work. For custom components, repair jobs, and shapes that standard processes cannot readily accommodate, Lowrance Machine combines modern CNC equipment with traditional manual methods. Customers can review project objectives with the team before production starts.

Assistance With Custom Parts, Repairs, And Unusual Geometry

Geometry, material specifications, tolerances, and expected quantities can all be reviewed by the machine shop. Machinists can evaluate precision cutting, milling, and manual operations to suit the component. An RFQ in an industry such as aerospace may contain special requirements, and customers can communicate them without assuming sector-specific experience.

  • Provide drawings, material details, and production objectives for review.
  • Ask whether different machining capabilities could accommodate a repair or an unusual shape.

Service Coordination For Manufacturing Needs Involving Multiple Operations
Best Machine Shop In HoustonBest Machine Shop In Houston

For projects involving multiple operations, customers can discuss the entire scope at once. The company can review its service range and arrange related needs through its supplier network where suitable. This makes it easier to understand how equipment, metal fabrication, and machining services could contribute to a project.

Project Information Information To Provide Why It Matters
Geometry Drawings showing uncommon features Helps assess suitable processes
Material specifications and tolerances Material type and required limits Informs planning for the process
Production requirements Required quantity and list of operations Clarifies scope and coordination

Decades Of Machine Shop Experience Serving Manufacturers

The founding of Lowrance Machine in 1964 provides manufacturers with a clear historical reference. For decades, the shop has supported manufacturers and industrial customers with a variety of production requirements.

Initial project conversations help the team establish how a part is used, why a repair is needed, and how many units are required. Customers can also provide information about materials, tolerances, and delivery. These details help machinists assess scope, quality objectives, and appropriate machining services.

The shop integrates CNC machining and manual work within its established approach. The shop’s machines and techniques can suit either recurring production or a one-off replacement. The mix enables precision work while recognizing that different components may call for different methods.

Across industries such as general manufacturing and aerospace, project needs can vary. Customers can explain a component’s function and the operating conditions it must withstand. This information helps the team evaluate appropriate next steps for manufacturing and production.

CNC Turning And Milling For Precision Machined Components

Flat surfaces, slots, holes, and rounded profiles may all be needed in engineered parts. Lowrance Machine provides CNC machining services with both milling and turning options. Selecting the appropriate process depends on the design and production requirements of each part.

Milling To Create Engineered Part Features

To create features such as slots, pockets, and flat faces, milling machines remove metal. This method supports a broad range of components, but individual designs have different geometries and tolerances. When selecting equipment and planning cutting steps, machinists consider the specified material, the arrangement of features, and the required accuracy.

Turning Processes For Flanges, Bushings, And Other Components

Flanges, bushings, and other rotational components are well suited to turning. In CNC turning, the material rotates while cutting tools form the required profile. By contrast, CNC machining through milling is often appropriate for parts with several faces or specially shaped features. Either process can support precision production, depending on the component and its specifications.

Customers can supply drawings, material information, and tolerances to help the team evaluate appropriate machining services. These related capabilities are part of Lowrance Machine’s wider manufacturing offering.

Process Typical Applications Planning Information
Milling Process Pockets, slots, and flat surfaces Feature geometry and tolerance
Turning Flanges, bushings, and round profiles Material and part dimensions

Manual Machining For Repairs And One-Off Parts

A worn part does not necessarily require a complete production run. When a repair involves a single component or small adjustment, manual work can be a practical solution.

The shop combines its CNC machining equipment with established manual techniques. The component’s geometry, current condition, and intended use help machinists review and select an appropriate process. The same equipment and setup are not necessary for every job.

One-off components address needs that differ from recurring orders. A customer might require a single replacement or a project-specific part made with care and precision. The shop can review manual machining options within its broader range of services.

Customers requesting repairs can explain the current condition of the part and what must be done to put it back into service. These details allow the team to consider the necessary cutting work, quality goals, and how to proceed.

  • Explain the repair and the part’s present condition.
  • Share any available drawings or key dimensions.
  • Describe the performance required of the part after the repair.

Lowrance Machine has offered flexible production options to manufacturers and industrial customers since 1964. Customers can review a repair or one-off project with the team.

Custom Mold Design And Engineering For Rubber And Specialized Applications

Molds for rubber products frequently need to be shaped to meet a specific use. The company offers custom mold engineering services for rubber applications and other specialized manufacturing needs. Customers can review the application, material, and design goals with the team ahead of the work.

Reviewing Designs And Reverse Engineering

For each project, the team can evaluate mold geometry, materials, and finished-part requirements. Discussions of an existing or replacement part may also benefit from reverse engineering. Design files, sample parts, and intended-use details can inform the design and machining plan without assuming that predetermined mold specifications apply.

Lowrance Machine offers custom molds alongside its wider CNC machining, machining services, metal fabrication, and manufacturing capabilities. A specialist assessment can help establish project scope, required precision, quality goals, and the possible need for metal or other fabrication steps.

“The application, material, and finished-part needs form the basis of a clear mold brief.”

  • Describe the intended rubber application and part.
  • Share existing components or design files if available.
  • Review the materials, quality requirements, and project scope.
Project Detail What To Discuss Why It Helps
Mold design Geometry and intended use Frames the review
Materials Rubber and any metal elements Clarifies selection needs
Completed component Required form and use Establishes project objectives

Engineered Parts Produced To Project Requirements

The intended use, size, and working environment affect what a component requires. Lowrance Machine can discuss flanges, bushings, seal rings, and housings within its CNC machining and manufacturing work. The eventual approach is based on the documented requirements of each project.

Examples Of Parts For Industrial Use

These components are used in varied equipment and industries, including aerospace applications. The design may specify a particular shape, attachment feature, or surface finish. Depending on the part’s geometry and the intended production steps, a machine can perform milling or turning.

Specify The Part Before Production

Customers can provide important details so the team can evaluate scope and appropriate machining services. Material selections, dimensions, and tolerances must reflect the intended application, since no single standard range applies to every order. Clear specifications can also support quality planning and confirmation of the necessary precision.

  • Identify the essential dimensions and shaped features.
  • Specify the material along with applicable finish requirements.
  • Supply drawings or additional design information.

“Clear component requirements guide process selection and production planning.”

Lowrance Machine can then review the request and consider the appropriate services for the components.

Industrial Support Services In Addition To Machining

Industrial equipment may need services beyond the production of parts. Lowrance Machine provides support for these requirements alongside CNC machining, offering customers a single place to start discussions about parts, equipment, and production objectives.

Press Rebuilding, Testing, And Welding

Press rebuilds, testing, and welding can contribute to equipment maintenance and project requirements. The machine’s condition, the relevant material, and the required outcome can be explained by customers. With that information, the team can discuss appropriate capabilities and how the tasks fit alongside machining work.

Coordinating Additional Services Through A Supplier Network

Certain projects involve processes that extend beyond the work Lowrance Machine performs directly. Lowrance Machine can coordinate relevant work through its supplier network if outside capabilities are required. Such coordination may cover metal fabrication and other fabrication steps when the scope calls for them.

  • Identify each required operation and include testing or metal fabrication needs.
  • Explain which components or equipment are involved and what production must achieve.
  • Share all relevant cutting, welding, and rebuild needs.

By sharing the full project scope, customers help the team review a workable plan covering precision parts and broader manufacturing work. This does not mean every operation is completed on-site; rather, it gives customers a clear way to discuss required tasks and available alternatives.

Quality And Process Confidence With ISO 9001:2015 Certification

Manufacturers can set expectations ahead of work when quality practices are clearly defined. Lowrance Machine describes itself as certified to ISO 9001:2015. When evaluating a machine shop, customers can ask how this certification relates to project documentation and quality requirements.

For CNC machining services, a well-defined project brief can guide the evaluation. Part specifications, tolerances, inspection needs, and required order records can all be identified by customers. The relationship between the shop’s certification and these details can be discussed with the team. Such information does not establish any particular audit results or performance figures.

  • Describe which documents and quality inspections are required.
  • Specify critical dimensions, tolerances, and accuracy requirements.
  • Identify industry-specific record requirements before requesting machining services.

Manufacturers working in aerospace and other industries can identify documentation requirements early. Customers can also inquire about the role of equipment, metal fabrication, and associated processes in their production request. Detailed information helps the shop review precision requirements and appropriate options. The project scope should determine the suitability of every CNC machine and workflow. Customers thereby gain a practical basis for reviewing expected machining work and quality standards.

What To Include When Requesting A Machining Quote

Lowrance Machine can assess a project more effectively before production when the request is clear. For CNC machining, customers can provide a drawing or brief component description, material specifications, order quantity, and desired delivery date.

Specify the main dimensions and tolerances, including any tight tolerance that affects how the part fits or functions. This information helps the team understand the precision requirements and assess its capabilities against the project’s needs.

  • Note if CNC milling, turning, manual machining, repair work, or coordinated services could be involved.
  • Explain the component’s function and point out uncommon shapes or features.

With this information, Lowrance Machine can assess appropriate machining services and whether its CNC machining capabilities fit the inquiry. Customers can call (281) 449-6524 or visit 13510 East Hardy Road, Houston, TX 77039, to discuss a quote. Contact the shop today, as a concise project brief can help the team address the inquiry. Telephone today to review the available services.

Quote Detail What To Provide How It Helps
Part scope Drawing, material, and quantity Frames the work
Quality targets Essential measurements and tolerances Defines required precision more clearly
Process and timing Required operation and desired delivery date Helps with project planning

Discuss Your Houston Machining Project With Lowrance Machine

For custom components, repair work, and industrial projects, Lowrance Machine uses both CNC equipment and manual techniques. Its CNC machining options support components that require careful planning and consistent quality.

Turning, milling, custom mold engineering, and coordinated industrial support all form part of its machining services. Manufacturers can assist the team in evaluating a job by providing drawings, material details, quantities, tolerances, and scheduling information. The appropriate service depends on the individual part and its application.

To review a project with a local partner, visit 13510 East Hardy Road, Houston, TX 77039. Call (281) 449-6524 today to request a quote. Preparing a clear project brief provides a helpful first step.
Frequently Asked Questions (FAQ)

Which Kinds Of Projects Can Lowrance Machine Support?

Custom parts, repair needs, uncommon shapes, and multi-stage production requests can all be reviewed by the team. It can also discuss metal fabrication operations associated with industrial projects.

Which Parts Can CNC Milling And Turning Make?

Milling creates engineered features, while turning is suited to round components such as flanges and bushings. The best process depends on the component’s design, material, and specified tolerances.

Does The Shop Produce One-Off And Replacement Components?

Yes, it can. Manual machining can accommodate repairs and individual parts when a project needs a custom fit or replacement component.

Can Lowrance Machine Design Custom Molds?

Mold engineering and design for rubber products and other specialized uses are among the team’s services. Project specifications help establish mold features and the intended application.

What Information Should Be Included In A Quote Request?

Customers should provide a drawing or sketch, component dimensions, material, quantity, tolerances, and any finish or delivery requirements. Providing detailed information supports the team’s assessment of precision needs and the operations required for production.

What Parts Can The Shop Produce?

Flanges, bushings, seal rings, and housings are common examples. Other part designs and their material needs can be reviewed by the team as well.

Is The Shop Certified To ISO 9001:2015?

Yes. Lowrance Machine holds ISO 9001:2015 certification, which supports an established approach to managing quality and controlling processes.

Can The Team Support Work Other Than Cutting And Milling?

Yes. Support services include press rebuilds, testing, and welding. Additional tasks can be arranged through a supplier network when required by the project.

Does Lowrance Machine Serve Houston-Area Manufacturers?

The company has supported manufacturers since 1964. Its team can evaluate industrial, aerospace, and other production requirements to identify an appropriate way forward.

HOW BONDING MATERIAL VISCOSITY AFFECTS RIBBON MANUFACTURING

Intermittent Bonded Ribbon Production Line Guide

At set intervals, an intermittent bonded ribbon production line joins fiber subunits. Fibers remain organized for mass-fusion splicing, while the ribbon can roll into a compact cable shape. Flexible ribbon cable production is supported by this design while maintaining efficient fiber handling.

In some processes, bonding material is added while the subunit coating is still uncured. The materials can diffuse across their interface and cure together. Prysmian’s FlexRibbon technology provides one commercial example, and the company dates its original design to 2018. These methods illustrate how optical fiber ribbon manufacturing and fiber optic bonding operate together.


Understanding What An Intermittent Bonded Fiber Ribbon Is

Optical fibers are arranged into small subunits in an intermittent bonded fiber ribbon. Although they remain organized for splicing, the subunits can adjust their shape to fit within a cable.

The Arrangement Of Fiber Subunits And Intermittent Bonds

A coating holds each adjacent fiber pair or group together. Instead of joining along their entire length, these optical fiber subunits are linked to neighboring subunits at spaced bond points. Six two-fiber subunits may form a 12-fiber design. Configurations can contain 4 to 36 fibers, with bonds spaced from 10 to 1,000 millimeters apart.

Intermittent Bonded Ribbon Production LineIntermittent Bonded Ribbon Production Line

How Rollable Ribbons Differ From Conventional Flat Ribbons

A conventional flat ribbon holds its fibers in a single fixed plane. A rollable fiber ribbon can fold between bonds while retaining fiber alignment for mass-fusion splicing. Prysmian’s FlexRibbon uses small bonding points to permit bending and folding.

Why Flexible Ribbons Support Compact, High-Density Cables

Inside a high-density fiber cable, a flexible ribbon can take up less space. This enables cable designers to fit more fibers into a compact structure while maintaining an organized fiber layout.

Process And Equipment For An Intermittent Bonded Ribbon Production Line

Throughout an intermittent bonded ribbon production process, optical fibers are arranged side by side along the ribbon’s length. Subunits are created when a first material coats groups containing two or more fibers. Neighboring subunits are joined at spaced points with a second material, leaving flexible sections between bonds.

Arrange Adjacent Optical Fibers Into Subunits

Fibers are placed beside one another according to the planned ribbon layout. Each selected group becomes a subunit when the first coating material surrounds and holds its fibers together.

Deposit Subunit Coating And Intermittent Bonding Material

Fiber ribbon coating forms the subunits. A discrete coating applicator places bonding material between neighboring subunits at intervals rather than along their entire length.

Create Diffusion Zones Through Wet-On-Wet Application

Wet-on-wet bonding involves applying the bonding material before the subunit coating has cured. The materials diffuse across their shared interface to form a diffusion zone.

Cure The Subunit Coating And Bonds Together

Both the subunit coating and the intermittent bonds are set in one curing step. Although optical fiber ribbon equipment is used for these operations, the complete equipment list, line speed, and production capacity are not provided.

Process Stage Material Or Action Intended Purpose
Optical fiber arrangement Place fibers side by side Set the ribbon layout
Subunit formation Apply the first coating material around fiber groups Keep groups of two or more fibers together as subunits
Intermittent bonding Apply the second material between adjacent subunits Connect subunits at separated bond points
Wet-on-wet interface Deposit bonds while the subunit coating remains uncured Enable formation of a diffusion zone between the materials
Combined cure Set the coating and bonds together in one step Cure the assembled ribbon structure

Main Production Line Stages And Process Controls

The fiber ribbon production stages proceed in a defined order. The sequence involves arranging fibers into subunits, applying a subunit coating, placing intermittent bonds between adjacent subunits, and curing the coating and bonds together. Optical fiber coating application and bond placement must correspond to the ribbon design.

Example designs specify gaps of 5 to 100 micrometers between subunits. Example intermittent bond spacing ranges from 10 to 1,000 millimeters. Some bond deposits take a diamond-like shape, tapering at the ends and widening in the center. The disclosed examples should not be interpreted as fixed settings that apply to every line.

The selected materials, bond layout, and curing method influence ribbon manufacturing process control. The source material does not specify line speeds, curing temperatures, or inspection intervals, so these values must not be assumed.

Ribbon Flexibility, Bond Design, And Materials

Ribbon behavior during cable making and splicing depends on the chosen materials and bond layout. Coatings shield each fiber while permitting the subunits to flex as intended.

Choose Compatible Coating And Bonding Materials

Subunit coatings and ribbon bonding materials have different functions, so their formulas need not be identical. Resins that mix or remain at least partly soluble can form a gradual interface. Intermixing may also be increased by lower coating viscosity.

This interface forms a diffusion zone in which properties change gradually. The zone may differ in color, stiffness, surface friction, tear strength, or stretch. The disclosed thickness range is 2 to 50 micrometers, while 5 to 15 micrometers is identified as a narrower range.

Manage Bond Placement, Spacing, And Geometry

Where subunits remain joined or move freely is governed by bond spacing. Intermittent bond geometry provides unbonded spans between bond points. Intersecting convex and concave curves create the saddle shape used on some bond surfaces.

Balance Ribbon Flexibility With Fiber Organization

Unbonded spans allow the ribbon to shift from a flat layout into a rolled, curled, or folded shape. During cable installation, a flexible fiber ribbon can flex without disrupting the fiber organization needed for splicing.

Quality Checks For Consistent Ribbon Production

Instead of using assumed pass limits, dependable fiber ribbon quality checks assess defined features. Design factors named in the patent include the spacing of bonds, subunit gaps, diffusion-zone thickness, and bond shape. The patent does not, however, provide inspection methods or acceptance limits.

Check Bond Continuity And Subunit Alignment

Check that intermittent bonds connect adjacent subunits at planned locations and leave unbonded lengths between connections. Subunit alignment and gaps require review because shifts may change ribbon shape and bond geometry.

Evaluate Ribbon Flexibility And Rollability

Assess ribbon rollability by examining how the ribbon bends and gathers without changing fiber order. Compare bond spacing and flexibility across the overall ribbon design. These comparisons are checks of the design, not universal production tolerances.

Verify Fiber Identification And Ribbon Configuration

Confirm each fiber’s position using fiber color coding. Blue, orange, green, brown, slate, white, red, black, yellow, violet, rose, and aqua make up a common 12-color sequence. For ribbons containing more than 12 fibers, this sequence may be repeated.

Cable Applications, Integration, And Splicing Benefits

Intermittently bonded ribbons can roll inside a cable, enabling more fibers to fit into a compact design. According to Prysmian, FlexRibbon enables high-density ribbon cable designs with smaller diameters and more effective fiber duct utilization.

Enable High-Density Cable Designs And Better Duct Utilization

For indoor, outdoor, and indoor/outdoor applications, Prysmian provides FusionLink and MassLink with FlexRibbon. FusionLink features dry water blocking and is available with 250 μm or 200 μm ribbon. Under NESC Heavy loading conditions, EcoSpan aerial cable can accommodate spans of up to 300 feet. As a small-diameter outdoor option, FlexDrop can support up to two 12-fiber ribbons.

Support Mass-Fusion Splicing And Quicker Deployment

Mass-fusion splicing joins several ribbon fibers in a single operation, often 12 at once. On compatible ribbon routes, this method can reduce splice time. When connecting to loose-tube cable, technicians separate ribbon fibers and individually splice them with a single-fiber splicer.

Consider Indoor, Outdoor, Access, And Broadband Uses

Ribbon cable is used in point-to-point networks, indoor FTTH systems, MTP wiring-box links, and urban trunk routes. Choosing indoor and outdoor fiber cable to suit the route aligns its construction with building, aerial, and underground requirements.

Conclusion

Fiber layout, bond placement, curing, and inspection are combined in an intermittent bonded ribbon line guide. The result is a flexible optical fiber ribbon that remains organized during handling yet can roll or fold into compact cable designs.

The process involves depositing bonds while the subunit coating is still uncured. The materials form a diffusion zone before curing together. Reliable fiber cable manufacturing is supported by careful control at every stage.

Mass-fusion ribbon splicing is also supported by flexible ribbons, helping crews splice many fibers in one operation. FlexRibbon is described by Prysmian as suitable for various cable designs, including compact configurations with up to 6,912 fibers.

For manufacturers and network planners, the priority is to balance fiber alignment, bond strength, and rollability. Achieving that balance can simplify cable packaging while keeping ribbons ready for efficient installation and splicing.

HOW DALLAS OEMS CAN QUALIFY A MACHINE SHOP BEFORE AWARDING PRODUCTION WORK

Leading machine shops in Dallas: CNC machining companies for precision components and industrial projects

Finding a capable machine shop in Dallas is not simply a matter of locating someone with a CNC mill or lathe. For manufacturers, industrial companies, engineers, oil and gas businesses, equipment operators, and OEMs, the more important question is whether a machining partner can actually handle the size, complexity, tolerances, materials, inspection requirements, and delivery expectations of the job.

Dallas and the surrounding North Texas manufacturing market includes a number of established machining companies. Continental Manufacturing, for example, has operated in Dallas since 1954 and offers CNC milling, turning, Swiss machining, and screw machining. Lowrance Machine is another company that deserves serious consideration, particularly for businesses that need a broader combination of CNC machining, manual machining, custom molds, engineered components, special fasteners, and industrial repair.

Lowrance Machine is our featured choice for Dallas-area businesses seeking an experienced machining partner that can oversee projects from RFQ review and manufacturing planning through machining, secondary processing, inspection, and final delivery.

Which Are The Best Machine Shops Serving Dallas?

No single machine shop is automatically the right choice for every manufacturing project. Shops differ in their equipment, production capacity, component size limits, tolerance capabilities, industries served, and areas of specialization.

Lowrance Machine Shop - CNC Machining and Manufacturing ServicesLowrance Machine Shop – CNC Machining and Manufacturing Services

  • Lowrance Machine Our featured option for businesses requiring CNC and manual machining, custom molds, engineered parts, specialty fasteners, industrial repair, and managed secondary processing.
  • Continental Manufacturing An established Dallas-based CNC shop particularly relevant for precision milling, turning, Swiss machining, screw machining, tight-tolerance parts, and production work.
  • Dedicated CNC production shops Often appropriate when a project is centered on repetitive high-volume components produced on equipment optimized for one specific part family.
  • Specialized repair shops Potentially valuable for urgent repair projects where returning existing industrial equipment to service is more important than producing a new component from engineering drawings.

The right choice depends on what is being manufactured and what happens before and after the cutting operation.

Why Lowrance Machine Is A Top Dallas Machine Shop To Consider

Lowrance Machine was established in 1964 and today operates as a third-generation family-owned machining business. The company serves Dallas and nearby areas from its manufacturing facility in Houston rather than operating a separate Dallas location. Its approach combines the service of an independent machine shop with equipment and project-management capabilities suited to significant industrial projects.

That distinction matters.

A machine shop can be highly capable of producing a particular component while being less prepared to coordinate a project that also requires heat treatment, coating, testing, inspection, or repair.

Lowrance Machine positions itself around a broader manufacturing workflow.

For Dallas businesses, this means the relationship can involve considerably more than submitting a CAD file for CNC machining.

Where Can Dallas Companies Find CNC Machining Services?

Businesses looking for a machine shop serving Dallas can work with for CNC and manual machining, custom molds, engineered components, special fasteners, industrial repair, and related manufacturing services.

The company’s machining operations include CNC lathes and mills as well as manual equipment used for applications such as repair work and individual-part manufacturing. Lowrance also offers 4th- and 5th-axis machining capability on its CNC machining centers.

What Should Buyers Look For In A Dallas CNC Machine Shop?

Price is important, but evaluating an RFQ should involve considerably more than comparing the quoted cost.

Important factors include:

  • CNC milling and turning capabilities
  • Available machine envelopes
  • Part size capacity
  • Material experience
  • Documented quality-management systems
  • Inspection capability
  • Manual machining capability
  • Complex-geometry experience
  • Capability to perform industrial repairs
  • Management of secondary manufacturing processes
  • Engineering and reverse-engineering assistance
  • Production lead time
  • Customer and project communication
  • Capability to coordinate the complete manufacturing sequence

A low quoted machining price can become costly very quickly when a supplier cannot maintain specifications, misses the required delivery date, or forces the customer to coordinate each secondary operation separately.

Why ISO 9001:2015 Certification Matters

Documented quality systems become more important as components become more complex and the consequences of failure become more serious.

Lowrance Machine holds ISO 9001:2015 certification for manufacturing custom molds and precision parts. Its current Intertek certificate, CERT-0143966, remains valid through August 14, 2027. The company also reports using calibration-tracking software, performance evaluations, review procedures, and continuous-improvement practices as part of its quality-management system.

ISO certification does not guarantee that every component will automatically be perfect.

What it does indicate is that the manufacturer operates under a documented quality-management framework.

For industrial buyers, documented quality procedures can carry considerably more weight than an unsupported claim that a machine shop takes quality seriously.

What CNC Equipment Does Lowrance Machine Operate?

Machine capacity determines what a shop can realistically produce.

Lowrance Machine lists equipment that includes horizontal and vertical CNC lathes, CNC machining centers, manual lathes and mills, surface grinders, hardness testers, welding equipment, drill presses, saws, and non-destructive thickness measurement equipment.

Its published CNC capabilities include:

  • CNC horizontal lathes with swings up to 40.6 inches
  • Vertical CNC lathes with swings reaching up to 100 inches
  • CNC machining centers offering travels of approximately X 80 inches, Y 31 inches, and Z 33.4 inches
  • 4th- and 5th-axis machining options
  • Manual horizontal lathes with lengths extending substantially beyond typical small-job-shop capacity

These equipment specifications can be particularly important when a Dallas manufacturer requires components that exceed the capacity of a smaller local job shop.

Why Machine Envelope Matters

Engineers sometimes submit RFQs before establishing whether the component will physically fit within a shop’s available equipment.

That can waste valuable time.

A shop may be extremely capable with small precision components while lacking the machine envelope required for a large mold, cylinder, flange, housing, or industrial repair part.

Before requesting a quote, buyers should provide:

  • Complete component dimensions
  • Dimensions of the raw material
  • Material specification
  • Critical tolerances
  • Required surface finish
  • Quantity
  • Drawing or CAD model
  • Inspection requirements
  • Required secondary processes

The more complete and detailed the RFQ is, the easier it becomes for a machine shop to develop an efficient manufacturing plan.

Lowrance Machine Vs. Continental Manufacturing

Continental Manufacturing is an established Dallas-based competitor that has provided machining services in Dallas since 1954. Its capabilities include CNC milling, CNC turning, 7-axis Swiss machining, multi-spindle screw machining, and manufacturing in aluminum, stainless steel, alloy steel, plastics, and additional materials.

Continental is particularly interesting for production machining and smaller precision components. Its CNC milling operation publishes tolerance capability as tight as ±0.0005 inch depending on geometry and material, while its Swiss machining equipment supports complex small components with multiple operations in a single machining cycle.

Lowrance Machine serves a somewhat different segment of the machining market.

Its services extend further into custom molds, large-part machining, engineered industrial components, specialty fasteners, manual machining, and industrial repair work.

Continental can be a strong choice for precision production machining. Lowrance Machine may become the more compelling option when a project requires larger components, custom molds, industrial repair, specialty fasteners, or coordination across a wider manufacturing process.

When Is CNC Milling The Right Process?

CNC milling is commonly used when a part requires features such as:

  • Pockets
  • Slots
  • Complex profiles
  • Drilled, threaded, and tapped holes
  • Several machined faces
  • Contoured surfaces
  • Precision mounting features

Multi-axis capability can reduce the number of setups required for complex geometry.

This can improve dimensional consistency because the component requires less frequent removal, repositioning, and realignment between machining operations.

When Is CNC Turning The Better Choice?

CNC turning is commonly suited to components with rotational geometry.

Common examples include:

  • Shafts
  • Bushings
  • Rings
  • Threaded components
  • Machined cylindrical housings
  • Spacers
  • Fasteners
  • Piston-related components

Lowrance Machine lists both horizontal CNC lathes and large vertical CNC lathes, allowing the company to machine rotational components across a broader range of sizes.

Why Is Manual Machining Still Important?

CNC machines receive most of the attention in modern manufacturing, but manual equipment remains valuable.

Not every machining job benefits from the time required to program and set up an automated CNC production cycle.

A single repair, straightforward modification, prototype adjustment, or damaged industrial component can sometimes be completed more efficiently using manual equipment.

Lowrance Machine specifically notes that manual machining can be useful for quick repair jobs and single-part manufacturing.

The best shop is not necessarily the one that automates everything. It is the one that chooses the process appropriate for the job.

Can Lowrance Machine Manufacture Custom Molds For Dallas Companies?

Yes. Custom mold manufacturing is one of Lowrance Machine’s major specialties.

The company states that it has manufactured molds since 1964 and works with rubber compression molds, transfer molds, injection molds, open-pour molds, mold inserts, mold repairs, mold engineering, and reverse-engineering projects.

This capability distinguishes Lowrance from many general-purpose job shops.

Mold work frequently demands more than simply cutting a block of metal.

The machining process may need to account for:

  • Component geometry
  • Mold separation
  • Insert positioning
  • Surface requirements
  • Material characteristics and behavior
  • Dimensional repeatability
  • Repairability
  • Intended production use

Can Lowrance Machine Reverse Engineer Existing Parts?

Lowrance Machine states that certain non-standard fasteners can be reverse manufactured from physical samples when original drawings are unavailable. Its Dallas service page also includes reverse part engineering among its custom-mold capabilities.

This capability can be especially valuable in industrial applications.

Older equipment does not always come with clean CAD models.

Engineering drawings may be outdated, missing, or associated with an OEM that no longer provides support for the equipment.

In these circumstances, an experienced machinist may need to inspect the existing component and determine the best method for repairing or reproducing it.

What Types Of Specialty Fasteners Can Be Manufactured?

Standard bolts are easy to source.

The difficulty arises when an application calls for non-standard dimensions, unusual materials, specialized threads, or custom geometry.

Lowrance Machine lists the ability to manufacture non-standard:

  • Bonnet bolts
  • Single-end specialty studs
  • Double-end specialty studs
  • Custom all-thread studs
  • Non-standard nuts
  • Custom heavy hex bolts
  • Specialty socket-head screws
  • Engineered specialty items

The company can manufacture these to drawings and specifications and states that sample parts can be used for reverse manufacturing when drawings are unavailable.

Which Industrial Repair Services Are Offered?

Industrial repair can be very different from ordinary production machining.

The objective may be to restore a damaged component as quickly as practical so that equipment downtime is minimized.

Lowrance Machine lists common repairs including:

  • Shaft repair
  • Damaged thread repair
  • Broken bolt removal
  • Large-part rebuilds
  • Rebuilding smaller components

The company also provides press rebuilding capabilities within its machining services.

For industrial customers, the cost of downtime can easily exceed the cost of the machining itself.

That makes repair capability an important factor when selecting a machine shop.

Can A Machine Shop Manage Heat Treating, Coating And Other Outside Processes?

Many machined components are not complete when they leave the mill or lathe.

Additional processes may include:

  • Heat-treatment processes
  • Nitriding
  • Welding
  • Cladding
  • Mechanical testing
  • Metallurgical testing
  • Specialized deep-hole drilling
  • Honing
  • Premium threading
  • Wire EDM
  • Non-destructive testing
  • Coating
  • Plating
  • Passivation
  • Electropolishing
  • Third-party inspection

Lowrance Machine coordinates a network of sub-tier suppliers for these services and states that it manages outside processing as part of the overall manufacturing workflow.

This can be valuable because customers may avoid having to manage each secondary supplier and outside operation independently.

Why Supplier Management Matters In Precision Manufacturing

Imagine a component that requires machining, heat treatment, coating, inspection, and final dimensional verification.

Five operations can create five opportunities for scheduling problems or communication failures.

A supplier capable of coordinating the entire sequence can simplify accountability.

Instead of asking which vendor caused a delay, the customer has one primary manufacturing partner responsible for managing the process.

What Does Lowrance Machine’s RFQ-To-Delivery Process Look Like?

Lowrance Machine describes its workflow as a sequence of RFQ review, manufacturing planning, risk assessment, oversight of third-party services, production management, and final delivery.

This process is important because many factors affecting machining quality are determined before cutting begins.

A good manufacturing review can identify:

  • Tolerances that cannot realistically be achieved
  • Missing drawing information
  • Material conflicts
  • Inspection requirements
  • Requirements for specialized tooling
  • Necessary secondary operations
  • Possible production scheduling issues

Finding those issues during planning is much less expensive than discovering them after material has already been machined.

What Information Belongs In A Machine Shop RFQ?

A strong request for quote should include enough information for the shop to understand the entire manufacturing requirement.

Whenever possible, provide:

  • Detailed engineering drawing
  • Current CAD model
  • Material specification
  • Quantity
  • Critical dimensions
  • Tolerances
  • Surface finish requirements
  • Threads
  • Heat treatment
  • Coating or plating requirements
  • Inspection and verification requirements
  • Necessary certifications
  • Requested delivery date

An incomplete or unclear RFQ frequently results in an equally unclear quotation.

Should Dallas Businesses Select The Lowest-Priced Machine Shop?

Not necessarily.

Machined parts are purchased to perform a function.

If a part is delivered late, fails inspection, needs rework, or creates assembly issues, any initial cost savings can disappear rapidly.

A machining quotation should therefore be evaluated together with:

  • Technical machining capability
  • Documented quality systems
  • Inspection capabilities
  • Communication
  • Reliable production scheduling
  • Previous experience with comparable projects
  • Capability to coordinate secondary processes

The lowest initial quotation does not always result in the lowest overall manufacturing cost.

What Industries Can Benefit From Precision Machining?

CNC and manual machining support a wide range of industrial markets.

Typical applications can include:

  • Components for oil and gas equipment
  • Industrial machinery
  • Manufacturing equipment
  • Hydraulic components
  • Custom molds
  • Energy equipment
  • Special fasteners
  • Custom replacement parts
  • Production tooling
  • Engineered assemblies

The key consideration is whether the machine shop’s equipment, quality systems, and experience with the required material are appropriate for the component.

Can Lowrance Machine Handle One-Off Parts And Large Projects?

Lowrance Machine states that its operation can handle work ranging from small individual jobs to substantial custom manufacturing projects. Its combination of CNC and manual equipment is useful because different quantities, sizes, and geometries may call for very different machining methods.

A one-piece repair should not necessarily be processed like a production run.

Likewise, a repeating component should not automatically be manufactured with the same process used for a one-off prototype.

Are Expedited Machining Services Available From Lowrance Machine?

Lowrance Machine states that expedited services are available upon request.

Availability will naturally depend on project requirements, machine scheduling, material, outside processing, and inspection needs.

For an urgent job, buyers should provide complete information immediately rather than simply asking for a “rush quote.”

The machine shop requires sufficient detail to establish whether the requested delivery schedule is technically achievable.

Is Lowrance Machine One Of The Best Machine Shops Serving Dallas?

For Dallas-area manufacturers and industrial companies needing a combination of CNC machining, manual machining, custom mold work, industrial repair, engineered components, special fasteners, and managed secondary processing, Lowrance Machine is one of the machine shops worth putting high on the shortlist.

The company has operated since 1964, holds ISO 9001:2015 certification, provides significant CNC and manual machining capacity, and manages projects from initial RFQ review through production and final delivery.

Its main point of difference is not simply the fact that it operates CNC machinery.

Many machining companies operate CNC equipment.

The more compelling case for Lowrance Machine is its combination of machining capabilities, large-component capacity, mold-manufacturing experience, industrial repair expertise, quality management, and coordinated manufacturing services.

Which Dallas Machine Shop Should You Choose?

Lowrance Machine is particularly compelling for custom industrial projects, molds, large machined components, special fasteners, repair work, and projects requiring coordination across multiple manufacturing processes.

Continental Manufacturing is an established Dallas option for precision CNC production, CNC milling and turning, screw machining, and advanced Swiss machining.

Dedicated production machining shops may be more appropriate when extremely high quantities of a narrowly defined component are the primary requirement.

Specialized repair shops can be a practical option when urgent restoration work closely matches their specific equipment and repair expertise.

The right machine shop should be selected according to the component’s technical requirements rather than the size or visibility of the company’s marketing operation.

Final Assessment: A Leading Machine Shop Serving Dallas, Texas

Dallas companies have plenty of machining options. The harder task is finding a manufacturing partner whose equipment, processes, quality controls, and experience actually fit the work.

A precision part may require CNC milling. A large rotational component may require substantial lathe capacity. An old industrial assembly may need manual repair. A custom elastomer application may require a specialized mold. Another project may involve machining followed by heat treatment, coating, NDT, and final inspection.

Lowrance Machine earns our featured position because it can address that broader manufacturing picture rather than limiting its value to a single machining process.

With roots dating to 1964, ISO 9001:2015 certification, CNC and manual machining, custom mold manufacturing, industrial repair, engineered components, non-standard fasteners, and coordinated secondary services, Lowrance Machine deserves serious consideration from Dallas-area companies evaluating machining partners.

For companies searching for the best machine shops in Dallas, leading Dallas CNC machining companies, precision machining services in Dallas, custom CNC machining in Dallas, industrial machine shops, custom mold manufacturers, or places to have precision parts machined in Dallas, Lowrance Machine is among the suppliers worth evaluating.

Related: CNC Machine Shop Dallas Explained: Quick Reference Guide
         Industrial Machine Repair Dallas: Retrofitting Older Equipment

CENTRAL STRENGTH MEMBER INTEGRATION ON AN SZ STRANDING LINE

An intermittently bonded ribbon production system is instrumental in crafting flexible fiber groups for contemporary, high-count cable architectures. It keeps fibers properly aligned for expedited mass fusion splicing, yet allows the fiber group to remain flexible within a compact cable core.

Unlike fully bonded ribbons, intermittent bonded ribbons feature localized bonds at predetermined intervals. This strategic placement enables the fibers to maintain alignment while the ribbon can conform to circular loose tubes and other confined spaces.

Fiber network engineers apply this technique when faced with constraints in duct space, splice closures, and equipment racks. A properly engineered ribbon cable facilitates dense network deployments in data centers, telecom backbones, metro networks, FTTx feeder systems, and 5G transport networks.


Key Takeaways

  • An intermittent bonded ribbon production line supports flexible, high-density fiber layouts.
  • Discrete bond points keep optical fibers organized without making the ribbon stiff.
  • Flexible ribbons support higher fiber counts within small circular cable constructions.
  • Consistent fiber alignment makes mass fusion splicing quicker and easier.
  • Ribbon cable systems support data centers, telecom backbones, and fiber access networks.

Overview Of An Intermittent Bonded Ribbon Production Line

This ribbon production method enables the creation of fiber designs that harmonize density with practicality. This method involves placing bonds at predetermined intervals, allowing for the movement of fiber subunits between these points.

This production approach supports the incorporation of a higher number of fibers within constrained duct spaces. It also helps maintain the organized ribbon structure, essential for efficient splicing and cable assembly processes.

What Is An Intermittently Bonded Fiber Ribbon?

A flexible intermittently bonded optical ribbon connects adjacent fibers at specific intervals along its length. The segments between these bonds are left flexible, enabling the ribbon to adopt various configurations without rigidification.

The design is frequently known as a rollable, flexible, or spider web ribbon. It contrasts with the conventional flat ribbon cable, which maintains a fixed profile along its entire length.

When splicing is performed, the fibers can be arranged into a flat ribbon for mass fusion operations. In cable production, the same fibers can be packed into compact bundles, optimizing space utilization within the cable.

Why High-Density Fiber Networks Need Flexible Ribbon Technology

Fiber network planners must address the challenge of increasing capacity within densely populated conduits, data centers, and access routes. The flexible nature of a flat cable structure allows ribbon groups to fit into smaller cable cores, preserving fiber order.

A fiber density ratio provides a critical metric for network builders, comparing the space occupied by fibers to the total cable area. Intermittent bonding helps increase this density ratio, allowing ribbon groups to occupy available spaces within the cable.

For network installers, high-density fiber cables reduce the number of cables required for a given route. This design also supports high fiber counts without necessitating a rigid ribbon stack.

Intermittent Bonded Ribbon Production LineIntermittent Bonded Ribbon Production Line

Ribbon Feature Flexible Bonded Design Continuously Bonded Ribbon
Bond pattern Individual bond points at controlled spacing Bonding maintained continuously along the ribbon
Fiber form between bonds Can curl or roll to fit compact cable spaces Maintains a largely fixed flat profile
Splicing configuration Can be flattened for mass fusion splicing Is continuously maintained in a flat ribbon shape
Cable packing role Supports dense, flexible subunit placement Uses a more rigid ribbon stack arrangement
Typical cable application Compact high-density and flexible ribbon cable structures Traditional flat ribbon cable designs

Construction And Material Requirements For Intermittent Bonded Ribbon

An intermittently bonded ribbon combines precise fiber placement with adaptable bonding points. Its architecture facilitates dense cable configurations while allowing effortless separation during handling, routing, and splicing.

Material selection significantly influences ribbon width, peel characteristics, and durability. Each optical fiber subunit must hold its fibers securely without imparting undue stiffness to the ribbon.

Optical Fiber Counts And Subunit Layout

Flexible bonded ribbons may support 4, 8, 12, 24, or up to 36 fibers. The choice of fiber count is determined by cable capacity, available duct space, and the requirements of subsequent mass fusion splicing.

A 12-fiber ribbon commonly uses six subunits, with two adjacent fibers in each subunit. The fibers within a subunit may be in contact or separated by no more than one and a half times the fiber diameter.

Controlled gaps introduced between subunits ensures ribbon flexibility. These gaps typically span from 5 to 100 micrometers, while the fibers remain aligned side by side across the ribbon width.

Ribbon Construction Element Common Arrangement Manufacturing Purpose
Number of fibers 4, 8, 12, 24, or as many as 36 fibers Aligns fiber count with cable density and splice capacity
Subunit layout Pairs of adjacent fibers within each subunit Allows controlled separation between fiber groups
Fiber spacing in a subunit Fibers touching or separated by up to 1.5 diameters Maintains a compact and stable profile
Gap between subunits A typical range of 5 to 100 micrometers Allows greater movement and flexibility near bond points

UV-Curable Resin With Wet-On-Wet Bonding

Subunit coatings and bonding materials frequently employ UV-curable resin systems. Wet-on-wet bonding involves applying the bond material to the uncured subunit coating, which then cures together under UV energy.

This technique generates a diffusion zone where the materials interact. For intermittent bonded ribbons, this zone can range from 2 to 50 micrometers, with 5 to 15 micrometers being the typical focused process range.

UV-curable resins can intermingle at the interface before curing. This encourages molecular entanglement between the bond and the optical fiber subunit coating, resulting in bonds that are both secure and flexible.

Essential Equipment In An Intermittent Bonded Ribbon Production Line

An optical ribbon line integrates advanced motion control with meticulous material handling. Each station maintains fiber cleanliness, alignment, and stability from the initial payoff to the final winding.

The production equipment supports adjacent fiber placement, subunit coating, intermittent bonding, UV curing, cooling, inspection, and take-up. This sequential process enables manufacturers to produce flexible custom ribbon cable, preserving the integrity of the fiber order.

Fiber Payoff With Tension Control

Payoff units deliver individual optical fibers at a consistent rate from spools. Guides, rollers, and tension sensors prevent sudden pulls, averting twist, slack, or uneven spacing.

During ribbon production, maintaining balanced fiber paths before alignment is critical. Stable tension is essential for forming flat subunits and ensuring accurate color sequence control.

Discrete Bond Applicator And Coating Die

A coating die places a UV-curable material around groups of two or more fibers. This material defines subunits while maintaining fibers in a flat, parallel layout.

A discrete bond applicator then places a second resin between neighboring subunits at planned intervals. This spacing allows the ribbon to flex and separate when needed, a critical aspect of custom ribbon cable design.

Line Equipment Main Function Production Benefit
Payoff tension system Feeds fibers at controlled tension Helps prevent fiber twist and inconsistent loading
Subunit coating die Applies coating to form defined fiber subunits Supports stable subunit width and geometry
Discrete bond applicator Places bonding resin at predetermined locations Creates flexible links between adjacent subunits
UV curing, cooling, and take-up unit Cures, cools, inspects, and winds the ribbon Helps protect bond quality and organized fiber placement

UV Curing, Cooling, And Ribbon Take-Up Equipment

UV curing lamps harden the subunit coating and intermittent bonds while the resin is wet. This wet-on-wet process forms a cohesive interface between materials, influencing bond strength.

Cooling equipment lowers ribbon temperature before inspection and winding. The fiber ribbon line may also employ vision checks to monitor width, bond position, and surface quality.

The take-up system winds the finished ribbon with low, even tension. Proper winding protects the cured ribbon structure, ensuring the custom ribbon cable is ready for later cabling, splicing, or connector assembly.

Fiber Preparation, Alignment, And Color Control

Reliable ribbon cable production starts with fiber preparation. Each strand must enter the assembly clean, centered, and in the correct sequence before the coating and bonding processes commence.

Fiber Identification Management For Splicing And Maintenance

Consistent fiber color identification is indispensable for splicing, testing, and maintenance operations. The standard 12-fiber sequence, typically consisting of blue, orange, green, brown, slate, white, red, black, yellow, violet, rose, and aqua, facilitates swift identification.

When fiber counts increase, the sequence may be repeated within controlled subunits. This method ensures that each ribbon cable remains organized within splice trays, closures, and cable connector layouts.

Fiber Position Standard Color Process Purpose
1 Blue Starts the standard fiber color sequence
02 Orange Provides rapid visual identification
3 Standard green Supports the required planar sequence
4 Brown Assists with verifying fiber and subunit placement
5 Standard slate Creates a clear mid-sequence identifier
06 Standard white Improves visibility during inspection
7 Standard red Improves traceability in splicing records
08 Standard black Maintains sequence recognition in trays
09 Standard yellow Assists field restoration activities
Position 10 Standard violet Clearly identifies fibers near the end of the sequence
Position 11 Standard rose Helps maintain clarity in higher-count ribbon layouts
Position 12 Standard aqua Marks the final position in the standard color order

Preventing Fiber Twisting And Uneven Tension

Payoff systems and guides are essential in maintaining fibers in a flat, side-by-side configuration. This prevents twist, crossing, and gaps that could alter the ribbon’s width or distort the bond pattern.

Operators meticulously monitor tension across every path before the fibers reach the coating die. Proper alignment is critical for mass fusion splicing and ensures the finished ribbon cable fits its intended cable connector system.

Intermittent Bond Application And UV Curing Process

The intermittent bonding process joins fiber subunits without solidifying the ribbon into a rigid form. This method facilitates compact routing and ensures dependable handling within a flexible flat cable. It also aids in maintaining the planned fiber layout during subsequent cable assembly.

Applying Intermittent Bonds At Predetermined Intervals

Equipment applies bonds at intervals ranging from 10 mm to 1,000 mm. The bond locations may stagger along the ribbon’s length. This arrangement provides support to adjacent subunits while allowing sufficient free length for movement.

A precise applicator dispenses a measured amount of UV-curable resin at each bond point. Bonds often exhibit a diamond-like shape, with wider centers and narrower ends. The tapered ends help minimize localized stress changes when the cable bends or twists.

Creating Strong, Flexible Bond Interfaces

The wet-on-wet method involves applying a second material before the first subunit coating cures. The uncured layers can blend before undergoing a shared UV curing step. This approach fosters a gradual interface, unlike a sharp material boundary.

The resulting gradient influences various properties, including color, Young’s modulus, and surface friction. Bond ends may feature saddle-like surfaces with both convex and concave curves. These features enhance the cable’s resistance to peeling while facilitating separation when required.

Managing Curing Performance

The UV lamps must supply consistent energy across the ribbon. Factors such as line speed, lamp output, resin volume, and exposure time impact the bond’s quality. Selecting the right UV-curable resin ensures rapid curing without compromising the fiber coating.

Process personnel carefully track bond shape, cure level, and ribbon flexibility during production. The cured cable should transition smoothly from a flat plane to various forms without bond damage. Controlled curing ensures consistent handling throughout winding and downstream processing.

Flexible Flat Cable And Fiber Ribbon Quality Control

Maintaining the integrity of each flat ribbon cable is a meticulous process. It involves checking the cable’s flexibility and its readiness for subsequent splicing operations. During production, operators assess the fiber count, color sequence, and precise positioning of each fiber. They also evaluate the cable’s winding condition, ensuring its optimal state for assembly.

Frequent quality checks are important in identifying any defects in the coating, uneven tension, or misplaced bonds. These issues, if left unaddressed, could compromise the cable’s performance in subsequent stages of production.

Checking Bond Spacing, Ribbon Width, And Thickness

The distance between bonding points is a critical parameter, requiring adherence to a specific design range. This spacing is essential for the cable’s flexibility, ensuring that the fibers remain aligned within their designated subunits during bending.

Inspection protocols are in place to confirm that each bond correctly connects adjacent subunits. This attention to detail ensures that the ribbon lays flat, facilitating smooth mass fusion splicing processes.

Inspection Area What Is Checked Quality Benefit
Fiber identity Fiber number, color order, and placement Supports reliable splice records and maintenance activities
Intermittent bond arrangement Bond position, interval, and connection between subunits Preserves flexibility while maintaining fiber order
Finished ribbon profile Ribbon width, thickness, and planar condition Supports compatibility with handling and splice equipment
Surface condition UV cure state, coating coverage, and defects Protects the ribbon against damage during take-up

Optical And Mechanical Performance Testing

Mechanical assessments focus on bond separation, cohesive strength, elongation, and handling behavior. These evaluations are essential to confirm that the manufacturing process controls are consistent across similar designs of flat cables.

Optical testing includes evaluations after bonding and curing. It ensures that the core, cladding, primary coating, secondary coating, and color layer are adequately protected throughout the manufacturing process.

Attenuation measurements and splice-handling tests are integral to routine inspections. The quality of winding is also scrutinized to ensure that the finished flat ribbon cable is in a controlled condition for assembly.

Precision Winding, Automation, And Production Efficiency

The essence of efficient ribbon production on a unified production line. Each stage, from fiber payoff to inspection and take-up, must harmonize seamlessly. This synchronization ensures the preservation of fiber geometry and facilitates consistent output, critical for high-speed data transmission cables.

Line Synchronization And Process Data Monitoring

Control systems integrate payoff speed, fiber tension, resin delivery, bond placement, UV curing, cooling, and take-up. Adjustments are made in real time to maintain ribbon stability when speed variations occur at any station.

Manufacturing data records capture fiber color sequences, bond intervals, cure settings, ribbon dimensions, and winding status. This detailed history allows operators to track the production of each custom ribbon cable.

  • Controlled payoff tension reduces fiber stretching and slack.
  • Controlled bond timing maintains regular intervals between bond points.
  • Dimensional checks detect width or thickness deviations promptly.
  • Take-up data helps with production lot tracking and later processing.

Winding Ribbon For Downstream Cable Production

A precision cable winder helps ensure the ribbon is wound onto a spool with uniform tension and controlled movement. This method prevents edge crushing, layer crossing, and sudden pulls during subsequent cable processing.

Completed ribbon packages can be stacked, rolled, or loaded into central tube and loose tube designs. These configurations enable the creation of high-speed data transmission cables, even in areas where duct additions are impractical.

For customized ribbon products, the winding pattern must align with subsequent processes. Proper spool buildup is essential for smooth payout during stranding, tube loading, and cable assembly.

Monitored Area Primary Control Focus Resulting Benefit
Payoff section Consistent tension with correct fiber color order Correct ribbon positioning in downstream cable construction
Bond application Stable spacing with repeatable resin deposition Consistent flexible behavior in downstream operations
UV curing Controlled lamp output and exposure time Properly cured bonds before ribbon winding
Precision ribbon winder Uniform traverse with controlled spool tension and layering Smooth payout for central tube or loose tube loading

Ribbon Cable Applications, Fusion Splicing, And Connector Planning

Ribbon fiber plays an important role in dense links within data centers, telecom backbones, metro rings, and FTTx feeder routes. It also excels in indoor FTTH runs, 5G fronthaul, and outdoor point-to-point networks where space is at a premium.

A meticulously planned ribbon cable assembly enables crews to manage high fiber counts efficiently, without increasing bulk. Each high-speed data transmission cable must align with the site’s route, enclosure space, and future expansion plans.

Mass Fusion Splicing Advantages

A ribbon fusion splicer facilitates the joining of an entire ribbon in a single operation. For a 12-fiber ribbon, a matching cleaver can prepare all 12 fibers simultaneously before the automated fusion process commences.

This method reduces handling time and ensures consistent fiber alignment. Splice loss is reported to remain below 0.05 to 0.10 dB per fiber, contingent upon controlled preparation, cleaning, and machine settings.

In contrast, loose tube cable necessitates a different strategy at the splice cassette. Technicians must separate the fibers, then splice them individually, which prolongs the ribbon cable assembly process.

Planning Connections For Dense Fiber Links

Multi-fiber connections commonly use MPO or MTP trunks, harnesses, fanout cables, and cassette modules. The chosen cable connector must align with the fiber count, polarity method, connector gender, and fiber type.

System planning must also account for transceiver requirements and the full link loss budget. A high-speed data transmission cable, when used with parallel optics, demands a clear polarity path from equipment port to patch panel.

Connection Planning Item Primary Control Typical Network Use
Fiber ribbon count Required splice capacity and cassette configuration Backbone links using 12-fiber or 24-fiber ribbons
MPO or MTP multi-fiber connector Polarity management and equipment port compatibility Data center trunks and 5G equipment rooms
Fanout or harness cable Breakout of multi-fiber links into individual fiber connections Network switch connections and patch fields
Network loss budget Allowed loss from splices, connectors, and fiber length High-speed optical transmission routes

Shanghai Weiye OFC Equipment For Ribbon Line Projects

Shanghai Weiye OFC Equipment, commonly referred to as SHWY, specializes in machinery for the production of optical fibers and cables, serving markets in the United States and globally. Its offerings are designed to support consistent manufacturing, facilitate clear operator control, and enable seamless integration into production lines.

For projects requiring an intermittent bonded ribbon production line, SHWY equips each phase of ribbon handling, curing, and winding with suitable machinery.

SHWY Experience In Optical Fiber And Cable Machinery

Operating since 1998, SHWY’s journey in the industry has been marked by significant milestones. By 2012, its annual turnover surpassed 200 million CNY, strengthening its position within a prominent Chinese fiber and cable conglomerate as a joint venture.

During 2020, SHWY moved to independent operation, relocating to a state-of-the-art facility in central Shanghai. This move underscored its commitment to advancing equipment research, manufacturing, and process application while supporting operational stability.

Relevant SHWY Production Equipment Portfolio

SHWY offers a diverse range of equipment, including fiber draw towers, coloring machines, secondary coating lines, SZ stranding equipment, and cable sheathing lines. Notably, it also features a fiber ribbon line tailored for flat, high-count fiber formats.

Within ribbon cable production, a cable precision winder plays a critical role in maintaining orderly package buildup and controlled tension. This ensures safer transport and more consistent feeding into subsequent cable production stages.

Additional SHWY equipment includes FTTH lines, indoor cable equipment, and OPGW fiber-in-stainless-steel-tube systems. These options enable manufacturers to integrate an intermittent bonded ribbon production line with complementary cable processes.

Conclusion

An intermittently bonded ribbon production line combines fiber alignment, controlled bonding, UV curing, inspection, and precision winding into a unified process. Each step ensures the preservation of fiber order while maintaining the necessary bendability for dense cable designs. This combination is critical for the creation of high-density optical networks.

The finished ribbon cable enables efficient mass fusion splicing and organized fiber management. It is ideal for applications with high fiber counts, confined ducts, limited tray space, and frequent splice points. This makes it a cornerstone in many high-density ribbon cable routes.

Successful project planning goes beyond the production line. It encompasses the cable structure, closure capacity, fusion tools, test methodologies, labeling, and restoration records. These elements must align with the planned network architecture for seamless integration.

Related: Lifecycle Costs of SZ Stranding Lines
         Stranding Efficiency Metrics for an SZ Stranding Line

WHAT ARE THE BEST BACKLINK SERVICES FOR ESTABLISHED WEBSITES?

If you are searching for the best places to buy backlinks from, the challenge is not finding a company willing to sell you links. Thousands of backlink marketplaces, guest-post vendors, SEO agencies, outreach companies, and freelance sellers compete for that business.

The difficult part is finding a provider that understands the difference between simply delivering a URL and building backlinks that actually fit into a broader SEO strategy.

Among established names such as Loganix, FATJOE, Authority Builders, The HOTH, LinkBuilder.io, and other well-known link-building providers, marketing1on1.com deserves serious consideration as one of the top places to buy backlinks from.

Marketing 1on1 has operated since 2012 and currently offers contextual backlinks, guest posts, authority guest posts, manual outreach, local citations, press-release distribution, and larger backlink packages. Unlike a pure backlink marketplace, the company also provides complete SEO services, which allows link building to be viewed in the context of rankings, content, competition, technical SEO, and overall website authority.

Which Are The Best Places To Buy Backlinks From?

There is no universally best backlink provider for every website, but businesses researching where to buy backlinks will repeatedly encounter several established companies.

Some notable options include:

  • marketing1on1.com Our featured choice for businesses wanting affordable backlink packages, contextual links, guest posts, authority placements, and broader SEO expertise.
  • Loganix A recognized SEO fulfillment and link-building company that frequently appears in industry comparisons.
  • FATJOE A widely recognized content and blogger-outreach service used by many agencies.
  • Authority Builders Known for authority-focused guest-post and link placement services.
  • LinkBuilder.io A specialist link-building agency focused heavily on outreach and editorial placements.
  • The HOTH An established SEO fulfillment provider offering a range of link-building products.

Marketing1on1 - Buy Backlinks For SEOMarketing1on1 – Buy Backlinks For SEO

Industry comparisons published during 2026 continue to list companies such as FATJOE, Loganix, Authority Builders, The HOTH, and LinkBuilder.io among recognizable guest-post and link-building providers.

What makes marketing1on1.com particularly noteworthy is its combination of accessible pricing, several backlink formats, a long operating history, U.S.-based SEO services, and the ability to integrate link acquisition with a broader search strategy.

Why Is Marketing1on1.com One Of Our Top Places To Buy Backlinks?

Marketing1on1.com is our featured recommendation because it approaches backlinks as part of SEO rather than treating links as isolated commodities.

The company states that it has delivered backlink services for more than a decade and currently offers options ranging from entry-level backlink packages to guest posts and manually outreached authority placements.

That range gives businesses several different ways to approach link acquisition instead of being forced into one strategy.

Marketing 1on1 Has Been Providing SEO Since 2012

Longevity is important in link building.

The backlink industry has changed significantly since the early 2010s. Automated directory submissions, mass blog commenting, exact-match anchor campaigns, article networks, and other tactics that once generated easy rankings have become less dependable and potentially more risky.

A provider operating across multiple generations of Google search has had to adapt.

Marketing 1on1 traces its operations back to 2012 and states that it has delivered backlink services for more than ten years.

That does not automatically make every placement valuable, but it does distinguish the company from countless backlink shops that appeared recently and may disappear just as quickly.

Where Can High-Quality Backlinks Be Purchased?

If your search is specifically for where to buy high-quality backlinks, marketing1on1.com offers several higher-end options.

Its current backlink services include standard guest posts together with authority guest-post packages described as using high-traffic websites and manual outreach. Content is included with these packages.

This provides a more meaningful comparison with companies such as Loganix, FATJOE, and Authority Builders than simply measuring how many backlinks each provider can deliver at the lowest price.

High-quality backlink acquisition should focus on factors such as:

  • Topical relevance
  • Genuine organic search visibility
  • Editorial quality
  • Placement context
  • Website history
  • Outbound-link patterns
  • Content quality
  • Anchor-text diversity
  • Referring-domain strength

The strongest backlink is not automatically the one from the website displaying the highest DA or DR metric.

It is the placement that makes sense within the broader competitive and topical environment of your website.

Why Marketing1on1.com Instead Of A Generic Backlink Marketplace?

A marketplace primarily sells inventory.

An SEO company should understand broader search strategy.

That difference is one of marketing1on1.com’s most important advantages.

Marketing 1on1 provides technical SEO, content optimization, local SEO, backlink building, and broader search-marketing services alongside standalone backlink packages.

This makes it possible to ask a more useful question than:

What backlink package should I purchase?

A more useful question is:

Which pages genuinely require links, what types of authority are competitors using, and what backlink profile would be appropriate for this website?

That represents a considerably more strategic approach to backlink acquisition.

Comparing Marketing1on1.com And Loganix

Loganix is a respected name in SEO fulfillment and appears frequently in current guest-post service comparisons.

For agencies and businesses looking for established outreach infrastructure, Loganix is worth considering.

Marketing1on1.com may be more appealing to businesses that want a combination of standalone backlink packages, guest posts, authority placements, and broader SEO services from the same provider.

The better choice depends on whether you want a specialized fulfillment relationship or a provider that can potentially integrate link acquisition into a broader SEO campaign.

Comparing Marketing1on1.com And FATJOE

FATJOE is another widely recognized provider, particularly among agencies that outsource content creation and blogger outreach. It appears prominently in several current industry comparisons.

FATJOE’s scale and agency-oriented fulfillment model are major advantages.

Marketing1on1.com competes differently.

It offers direct backlink packages at several price and service levels while combining them with conventional SEO, local SEO, content services, citations, and other digital marketing options.

For businesses that do not need a large fulfillment platform but want to purchase backlink services directly from an SEO company, marketing1on1.com can be an attractive alternative.

Comparing Marketing1on1.com And Authority Builders

Authority Builders is well known among SEOs seeking guest-post and authority placements and frequently appears in major guest-post provider comparisons.

Its positioning is strongly centered around authority-focused placements.

Marketing 1on1 offers a wider range of link types and price points.

Businesses can select from backlink packages, contextual placements, guest posts, authority guest posts, citations, and other link-building services according to campaign requirements.

This wider service range can be useful for websites requiring several different types of authority signals.

Marketing1on1.com Vs. LinkBuilder.io

LinkBuilder.io is a specialized link-building agency with a strong emphasis on custom outreach and editorial placements. Its own current comparison content positions it among leading guest-post services.

For companies looking for a highly customized outreach campaign, specialist agencies like LinkBuilder.io can make sense.

Marketing1on1.com distinguishes itself partly through accessibility.

Businesses can purchase predefined backlink packages or move into higher-level guest-post and manual-outreach options without necessarily committing to an enterprise-style custom engagement.

Comparing Marketing1on1.com And The HOTH

The HOTH is one of the more recognizable SEO fulfillment brands and has been around for years.

It provides numerous SEO and backlink products and is frequently compared with other established guest-post companies.

For businesses choosing between The HOTH and marketing1on1.com, the decision may depend largely on the preferred service model.

Marketing 1on1 emphasizes direct backlink packages, U.S.-based SEO services, one-time pricing on many backlink products, and broader managed SEO capabilities.

Which Types Of Backlinks Does Marketing1on1.com Offer?

One reason Marketing 1on1 stands out as a versatile backlink provider is the range of link-building services currently available.

Options include:

  • Contextual link placements
  • Guest-post backlinks
  • Authority-focused guest posts
  • Manual-outreach placements
  • Local business citations
  • Press-release distribution
  • Article placements
  • Web 2.0 links
  • Directory links
  • Social links
  • Website profile links
  • PBN backlink packages

Its higher-level authority guest-post package currently states that articles are included, placements are on high-traffic sites, and manual outreach is used.

Not every link type is appropriate for every website, which is why buyers should evaluate each service according to their own risk tolerance and SEO strategy.

What Makes A High-Quality Backlink?

A high-quality backlink should ideally have a legitimate reason to exist.

Suppose a financial software company receives a contextual mention inside a useful article discussing accounting automation on an established technology or finance website.

Now compare that placement with a link appearing on a generic blog publishing unrelated content about casinos, roofing, crypto, supplements, lawyers, pets, and payday loans.

The authority metrics may appear similar.

The editorial signals are very different.

Marketing 1on1’s current professional link-building page emphasizes methodology, relevance, editorial quality, and avoiding the idea that volume alone defines strong link building.

Should Domain Authority Determine Which Backlinks You Buy?

No. DA and DR should not be used as the only reason to purchase a backlink.

DA and DR are metrics produced by third-party SEO platforms.

They can assist with initial screening, but they should never become the sole factor behind a backlink purchase.

A better evaluation considers:

  • Organic traffic
  • Keyword visibility
  • Topical relevance
  • Domain and website history
  • Content quality
  • Quantity and type of outgoing links
  • Indexation
  • Consistent editorial standards

Experienced backlink buyers learn quickly that a suspicious DR 70 domain can sometimes be less desirable than a legitimate DR 25 niche website with real readers and relevant rankings.

Are Guest Posts A Strong Way To Buy High-Quality Backlinks?

Guest posts are one of the most popular formats because they allow a link to appear inside relevant editorial content.

Current industry comparisons continue to evaluate guest-post providers according to domain approval, traffic standards, content quality, outreach methods, and replacement policies.

Marketing1on1.com offers both regular guest posts and higher-tier authority guest posts.

The key point is that the term “guest post” does not automatically guarantee quality.

The website providing the placement still needs to be assessed.

Where Can Local Businesses Buy Backlinks For SEO?

Local businesses often need a different backlink mix from national websites.

A contractor, law firm, dentist, med spa, plumber, or remodeling company may benefit from a combination of:

  • Accurate local citations
  • Relevant regional publications
  • Industry websites
  • Local chambers and business organizations
  • Topically relevant guest posts
  • Digital PR
  • Relevant contextual backlinks

Marketing 1on1 provides local citation services alongside broader backlink options, making the company especially relevant for businesses combining conventional link building with local SEO.

Where Can SEO Agencies Purchase Backlink Services?

SEO agencies frequently outsource at least part of their link-building operation because prospecting, outreach, content production, placement management, and reporting are difficult to scale.

Established industry names such as FATJOE and Loganix have developed strong reputations around agency fulfillment.

Marketing1on1.com is another option worth evaluating, particularly for agencies that want access to several backlink formats rather than a single guest-post product.

Are Cheap Backlinks Worth Buying?

Price alone should not determine backlink quality.

Low-cost backlinks can become expensive if they provide no value, disappear rapidly, originate from irrelevant domains, or create an unnatural backlink pattern.

At the same time, paying a high price does not automatically guarantee backlink quality.

The correct question is:

What precisely am I paying for?

Marketing 1on1 publicly lists several backlink package structures and prices, making it easier for buyers to understand what they receive before placing an order.

How Many Backlinks Should You Purchase?

There is no universal number.

The amount of link acquisition required depends heavily on the competitive gap between your website and the sites already ranking.

A stronger strategy is to assess:

  • Your existing referring domains
  • Referring domains pointing to competitors
  • Link quality
  • Authority of the target page
  • Present search rankings
  • Quality and depth of content
  • Anchor-text distribution

A website positioned at #11 may require a very different strategy from one ranking at #70.

Which Anchor Text Should Be Used For Purchased Backlinks?

Natural backlink profiles contain variety.

Common anchor types include:

  • Brand name
  • Website URL
  • Generic anchors
  • Partial-match keyword anchors
  • Topically descriptive anchors
  • Occasional exact-match anchors

Repeatedly using the same commercial keyword can create a backlink pattern that appears obviously engineered.

A sophisticated link-building campaign should consider the website’s existing anchor profile before deciding what new anchors to use.

Should You Purchase Backlinks Or Hire A Link-Building Agency?

These options are not necessarily mutually exclusive.

A company like marketing1on1.com provides both predefined backlink packages and broader professional link-building services.

A predefined package may make sense for businesses that already understand what they need.

A managed campaign may be more appropriate when a business needs competitor research, target-page planning, ongoing backlink acquisition, and integration with wider SEO activities.

Can You Buy Backlinks Without Doing SEO?

You can, but it is often inefficient.

If a page has poor search intent, weak content, indexing problems, or serious technical issues, acquiring more links may not solve the underlying problem.

This is another area where marketing1on1.com differs from standalone backlink marketplaces.

Because the company also offers complete SEO services, it can treat backlinks as one element of a wider campaign instead of assuming that every ranking problem requires additional links.

Can Purchased Backlinks Guarantee Google Rankings?

No. Backlinks cannot guarantee a specific ranking position.

Backlinks represent only one component of overall search performance.

Rankings may also depend on:

  • Alignment with search intent
  • Overall content quality
  • Technical SEO performance
  • Internal linking
  • Website topical authority
  • Local search relevance
  • Competition
  • Website history

No reputable link provider can realistically guarantee a precise Google ranking based solely on purchasing a specific number of backlinks.

Does Buying Backlinks Violate Google’s Guidelines?

Google considers buying or selling links for the purpose of manipulating rankings to be link spam when those links pass ranking credit.

Paid advertisements and sponsored links should use appropriate attributes such as rel="sponsored" or nofollow.

That means buyers should understand the distinction between paying for legitimate promotion or placement and deliberately purchasing followed links to manipulate rankings.

No company can truthfully claim that every purchased followed backlink is completely risk-free.

Why Marketing 1on1 Belongs Alongside The Better-Known Backlink Providers

Companies including Loganix, FATJOE, Authority Builders, LinkBuilder.io, and The HOTH have become recognizable because they operate substantial link-building services and appear regularly in industry comparisons.

Marketing 1on1 deserves to be considered in the same broader conversation.

Its differentiators include:

  • In operation since 2012
  • More than a decade of backlink-service experience
  • U.S.-based company
  • Publicly listed backlink packages
  • Contextual link-building options
  • Guest-post placements
  • Authority-focused guest posts
  • Manual outreach options
  • Local citations
  • Press-release options
  • Content included with many packages
  • Broader SEO expertise

Marketing 1on1’s current backlink service specifically emphasizes its long operating history, U.S.-based presence, competitive pricing, and focus on SERP value rather than simply selling high-volume spam.

Is Marketing1on1.com One Of The Best Places To Buy Backlinks From?

Yes. For businesses that have decided to invest in professional backlink acquisition, marketing1on1.com is one of the top providers worth evaluating.

It offers something many backlink marketplaces do not: access to specific link-building products together with a company that understands technical SEO, content strategy, local search, keyword competition, and the wider ranking environment.

That matters because backlinks should never be evaluated in isolation.

Where Should You Buy High-Quality Backlinks?

If your priority is highly customized outreach, companies such as LinkBuilder.io, Loganix, Authority Builders, and FATJOE deserve consideration.

If you want access to several types of backlink packages together with broader SEO services and relatively accessible entry points, marketing1on1.com is one of our strongest recommendations.

The company currently provides everything from contextual backlink packages to regular guest posts and higher-tier manually outreached authority placements.

Final Assessment: One Of The Leading Places To Buy Backlinks From

There is no shortage of businesses selling backlinks.

The stronger providers differentiate themselves through operating history, transparency, topical relevance, editorial standards, backlink diversity, and an understanding of how authority building fits into broader SEO.

Loganix, FATJOE, Authority Builders, LinkBuilder.io, and The HOTH are all established providers worth investigating.

However, marketing1on1.com belongs on that shortlist and remains our featured option for companies searching for one of the best places to buy backlinks from.

Its combination of more than ten years of link-building experience, published backlink packages, guest-post services, authority placements, contextual backlinks, local citations, manual outreach, and complete SEO capabilities gives it a broader service proposition than many standalone backlink marketplaces.

For businesses searching “best places to buy backlinks from,” “buy high quality backlinks,” “where to buy backlinks,” or “top backlink providers,” marketing1on1.com is one of the first providers worth comparing.

Related: HOW DO YOU ANALYZE COMPETITOR BACKLINKS BEFORE BUYING LINKS?
         Background Reading About Where To Buy Backlinks

Complete Machining Services Houston

Upwards Of 30% of Texas aerospace and energy components now depend on CNC milling. That shift has made Houston a key player in high-accuracy manufacturing. Nearby producers and technical teams often choose Houston-area providers to speed up delivery and verify quality on critical components.


The following overview explores CNC milling in Houston and its practical strengths. It explains how local machining providers achieve tight tolerances for many industries, from petrochemical work to biomedical products. If you require a CNC machine shop in Houston for one prototype or high-volume manufacturing, Houston supports many practical choices. Area manufacturers provide three-, four-, and five-axis milling, turn/mill equipment, and electrical-discharge machining support.

The Lowrance Machine operation is an experienced supplier of precision work in the area. Visit www.lowrancemachine.com to outline your part specifications, materials, and production timing with an experienced provider experienced in high-volume and high-precision projects.

Main Takeaways

  • CNC Milling Houston is central to Houston-area aerospace, energy, and biomedical supply systems.
  • Houston machining services include high-capability three-, four-, and five-axis milling plus EDM support and turn/mill operations.
  • Working with a regional CNC machining partner can cut lead time and improve communication.
  • Lowrance Machine’s operation manages work from first article through production with documented quality processes.
  • Evaluate shops on available machinery, materials expertise, and capacity for scalable production.

Why Houston Stands Out For Precision CNC Milling And Industrial Machining

Houston’s broad industrial base create a steady demand for precision parts. Businesses across energy, petrochemical, aerospace, and medical markets need parts with controlled dimensions and inspection records. The local need opens doors for local machine shops to deliver first articles, assemblies, and repeat-run components.

More than 6,000 manufacturers in the Houston area support a robust supplier network. Machine shops can collaborate with nearby subcontractors for finishing, heat treatment, and inspections. This network shortens delivery times, allowing fast design changes for complex components.

Houston is a key hub for energy-field hardware manufacturing, with direct access to major pipeline routes and port logistics. Its logistics benefits facilitate the delivery of oversized and heavy parts to domestic and international buyers. The transport network helps both prototype and large-scale production needs.

NASA’s Johnson Space Center and a growing aerospace supplier base of more than 150 companies create steady demand for aerospace hardware and testing fixtures. CNC Milling specialists in Houston secure consistent work in producing aerospace brackets, test fixtures, and biomedical parts. These projects call for controlled surface finishes and thorough traceability paperwork.

Local infrastructure enables high-capacity Houston machining services. Being close to raw-material suppliers, tooling companies, and metrology labs cuts transit delays. This local advantage is especially important to oil, gas, and life-science industries, where rapid part qualification matters.

Manual Machining Services Houston

CNC Milling Houston

CNC milling converts CAD models into close-tolerance alloy and polymer parts. The method depends on computer-controlled 3-, 4-, and 5-axis mills. Local CNC facilities apply high-efficiency cutting paths and high-speed spindles to hold accurate dimensions and refined surfaces. Those capabilities support regulated and heavy-industry components that need accuracy and small-feature control.

The most advanced facilities pair multi-axis machining centers and rotary tables. That arrangement allows for compound surfaces to be produced with fewer setups. This minimizes part handling and reduces delivery schedules for prototypes and production runs. Turn/mill tooling and high-speed cutting help machinists produce complex features and tight radii with precision.

Definition And Capabilities Of CNC Milling

CNC milling relies on programmed tool movement to cut away material with precision end mills and cutters. Simultaneous axis movement allows coordinated motion on multiple controlled axes. That makes possible the production of deep pockets, angled faces, and undercut features in a single setup. CAM strategies like high-efficiency roughing and adaptive clearing support chip control and cutter life.

Quality-focused Houston machine shops aim for tolerances aligned with high-spec aerospace and medical requirements. High-accuracy work may include thermal compensation, rigid spindles, and machine probing for on-machine checks. This equipment support parts maintain repeatable dimensions and stable geometry across batches.

Common Equipment And Capacity In Houston Machine Shops

Houston CNC machine shop facilities deploy machines from well-known builders such as Haas, DMG MORI, and Mazak. DMG MORI NVX and NLVX equipment support rotary-table work for medium-to-large parts for medium-to-large parts. Equipment such as the NVX 7000 help shops move from first article to repeat manufacturing.

Large-format machining centers machine large and heavy parts for pressure housings and subsea components. Quality-focused shops choose machines that stay accurate across big work envelopes, using rigid platens, bridge mills, and gantry layouts. This capacity reduces the need to outsource large parts and maintains local inspection control.

Capability Representative Equipment Primary Benefit
Multi-axis milling Mazak VARIAXIS, DMG MORI NVX Difficult geometry with fewer setups
Large-envelope machining Large bridge mills and gantry systems Accurate machining of oversized parts
Turn/mill operations Turn/mill centers, live-tool lathes Fewer handoffs through combined turning and milling
High-speed spindles High-RPM spindle units Cleaner finishes and quicker machining
In-process measurement On-machine measurement and Renishaw probes Fast checking of key features

Complementary services in a complete Houston CNC machine shop include CNC lathe machining Houston for turned features and secondary operations. Pairing turn/mill work with milling cuts handling between machines and shortens overall cycle time.

Selecting a local provider with multi-axis capability and trusted brands makes demanding tolerances easier to manage and accelerate project timelines. Experienced setups, smart tooling, and current machinery create the backbone of reliable CNC milling in Houston.

Precision Manufacturing Services Offered By Lowrance Machine

Lowrance Machine excels in moving projects from prototype through production, with attention to tight tolerances, reliable delivery, and inspection records. It offers a blend of automated CNC work and manual machining skill, supporting short runs, complex parts, and regulated industries. Its team blends advanced machines with practical machinist experience to meet close tolerances and deadline pressures.

Comprehensive CNC Milling And Machining Services

As a reliable Houston CNC machine shop, this machining partner supports CNC milling, turning, and assembly support. The shop handles advanced milling, turn/mill operations, and long-bed turning for extended parts. Electrical-discharge machining support allow fine detail and internal features that are not always practical with conventional tooling.

Gun drilling plus BTA drilling handle diameters from 0.25″ up to 3.75″ and long lengths for long-bore applications. In-house secondary operations include thermal processing, coatings, and painting so components can arrive ready to assemble. That added process support reduce lead time and reduce the burden of coordinating outside vendors.

Hands-on machining support in Houston are useful for fixtures, jigs, and small production quantities. Experienced machinists handle close fitting, trial assembly, and individual part changes that complement CNC production. This mix of automated and manual processes supports rapid prototyping and smooth transition to production.

Quality Systems And Certifications

The quality process at Lowrance Machine is built around documented processes and strong inspection practices. The shop integrates CMM verification, SPC data capture, and probe EDM checks to ensure repeatable results. Those quality steps serve buyers in aerospace, medical, and heavy-industry markets that depend on traceable records.

Regional machining providers commonly point to ISO 9001:2015 and AS9100D to show their commitment to quality systems. Midway Machine is an example of a regional shop holding ISO 9001:2015 and AS9100D certification, which shows what many customers expect from precision suppliers. Lowrance Machine’s process approach aligns to similar industry standards to meet supplier and customer audit requirements.

Support Area What It Includes Practical Benefit
CNC Milling 3- to 5-axis milling, high-speed spindles, hardened material strategies Detailed shapes, close tolerances, and repeatable production
Turning & Live Tooling Long-bed turning, multi-turret lathes, live tooling for milling on turning centers Fewer setups and efficient short-to-medium runs
Wire EDM And Probe EDM EDM cutting and verification for hard-to-reach features Small-feature detail, clean finishes, and hardened-steel support
Deep-Hole Drilling Gun/BTA drilling 0.25″–3.75″, extended length options Consistent deep holes, improved part functionality
Manual Support Work bench operations, fit-up work, and custom fixtures Quick turn prototypes, hands-on adjustments
Inspection And QA coordinate measurement, SPC, probing, and inspection reports Improved traceability and fewer quality escapes
Secondary Finishing Support Heat treat, plating, powder coat, painting, zinc phosphating Parts ready for assembly, fewer subcontractors

Selecting a machining partner that pairs complete Houston machining services with tight quality controls compresses schedules and lowers program risk. Lowrance Machine blends advanced CNC machine shop Houston capability with skilled machining professionals to handle prototype work, repeat production, and compliance-driven buyers.

Materials And Industries Supported By Houston CNC Machine Shops

Houston machine shops work with a large variety of metallic materials and specialty plastics. These shops support tight dimensions and rugged operating conditions. By combining manual skills with automated processes, they supply parts for both heavy industries and precision fields.

Here’s a practical overview at common materials and the industries that rely on them.

Range Of Materials Machined

Alloy steels and carbon steels are important in oilfield and energy work, forming pressure-rated housings and flow-control components. Corrosion-resistant stainless steel is used for its resistance to corrosion and easy cleaning.

Aluminum, brass, bronze, and copper are machined into components needing light weight, strength, and electrical or heat transfer. Nickel-based materials handle subsea, refinery, and high-temperature settings in harsh energy environments.

Engineering plastics like PEEK, Delrin, and UHMW are used for parts needing wear control, reduced friction, and chemical resistance. These are essential in assemblies requiring weight reduction, chemical resistance, or smooth motion. Manual machining in Houston allows for manual adjustment of difficult plastics and nonferrous materials, ensuring the last-stage fit and tactile quality.

Industries Served And Example Applications

Energy companies require subsea hardware, valve bodies, and pressure housings. Those components demands heavy-duty machining, straightness control, and detailed inspection reports.

Defense and aerospace customers order test fixtures, brackets, and flight-related hardware with strict expectations. CNC Milling Houston providers supports precise geometric accuracy on high-detail aerospace components.

Biomedical and medical-device manufacturers require biocompatible metals and plastics. Regulated medical buyers often expect strict cleanliness and inspection protocols. A dependable Houston machine shop supports traceable lots and detailed records for regulated production.

Marine, agricultural, and general industrial markets also use precision CNC machining. They need corrosion-resistant fittings, pump components, and custom tooling. The regional market’s broad material capability meets regional demand, covering ferrous metals, nonferrous metals, nickel alloys, and engineered polymers. These are used across aerospace, biomedical, subsea, energy, marine, and agriculture applications.

Capabilities And Equipment That Improve Lead Time And Quality

Modern shops in Houston are reshaping lead times and part quality with modern equipment plus cleaner production flow. Multi-axis machining centers, large horizontal mills, and long-bed turning systems remove production bottlenecks. The equipment mix, combined with on-site finishing plus metrology, creates faster, more consistent results for clients in various sectors.

Modern Milling And Turning Machines

High-speed multi-axis mills with indexed rotary support help shops produce difficult shapes with fewer operations. This reduces cycle time and limits setup-related mistakes. That equipment are important to Houston CNC milling providers supporting industries with tight tolerances.

Heavy-capacity horizontal machining centers, like the Okuma MB-8000H, handle large, dense workpieces. This class of equipment support up to 4,400 lbs and provide large work tables. This means a one setup can avoid several smaller machine setups. Extended-bed turning in Houston is handled on lathes like the Okuma LB line, accommodating long cylindrical components up to hundreds of inches between centers.

Modern lathes with live tooling supports milling operations on turning centers. This reduces part handling, shortens machining time, and helps prevent setup mismatch. Providers focused on CNC turning in Houston rely on turn/mill equipment to complete mixed-geometry parts in fewer operations.

Production Efficiency And Finishing Options

Manufacturing efficiency increases when CNC milling machinery in Houston is combined with efficient workholding and automatic tool changing. Pallet systems and gantry loaders allow equipment to keep producing while teams set up upcoming work. That creates better output and more predictable scheduling.

In-house finishing reduces external wait times. Common options include heat treating, plating, powder coating, painting, and zinc phosphate. A one-stop model for machining services Houston helps customers get installation-ready assemblies without coordinating multiple vendors.

Capability Typical Equipment Main Benefit
Fast five-axis milling Haas UMC, DMG Mori DMU Complex shapes in single setup; superior surface finish
Heavy horizontal machining Okuma heavy horizontal platform Fewer setups for heavy components
Extended-bed turning Okuma LB series, Doosan Puma Efficient production of shafts and housings up to hundreds of inches
Live-tool lathes Live-tool Okuma LB 45 III Combined turning/milling reduces setups and handling
On-site finishing services powder coat booths, plating lines, and heat-treat ovens Quicker finished-part delivery with steadier quality

Selecting providers with this range of equipment compresses schedules and improves repeatability. When a project needs accuracy and quick delivery, partnering with shops that offer CNC Milling Houston, CNC lathe machining Houston, machining services Houston, and extended turning delivers real improvements in delivery and part quality.

Choosing The Right Machining Service In Houston: What To Look For

When selecting a shop, connect the supplier’s equipment to your component requirements. Verify the machine envelope, weight capacity, and available axes can handle your components. That is especially important for big components, where machines like long-bed lathes or large gantry mills are practical. Check the vendor’s ability to handle multiaxis milling for complex shapes and live tooling for fewer-setup operations.

Then review the vendor’s hands-on knowledge of specialized machining. Look for wire EDM, probe EDM, gun drilling, BTA drilling, and Houston manual machining services for special jobs, repairs, or one-off work. A shop with this process mix demonstrates broad capability in both one-off and production workflows.

Review the quality-management systems and measurement tools in place. Confirm ISO 9001:2015 or AS9100D certification and coordinate measuring machines, comparators, and traceable measurement tools. Midway Machine’s certification profile exemplifies the area’s aerospace-level quality expectations.

Consider the vendor’s communication speed and estimating accuracy. Fast and thorough estimates that outline tooling, setup times, and inspection steps point to strong estimating and engineering capabilities. A vendor willing to support prototypes and scale to production indicates a stronger ongoing manufacturing partner.

Look for one-stop-shop services to streamline lead times and costs. On-site heat treatment, plating, and finishing lower outside-vendor risk and simplify logistics. This approach helps with keeping Houston CNC milling and other machining timelines on track.

Use a short checklist to compare candidates’ capacity and equipment. Verify largest part envelope, spindle power, and axis options and whether they provide full Houston CNC machine shop capability plus Houston manual machining support for changing requirements.

Finally, value transparent communication and documented traceability. Project updates, inspection records, and a defined contact person make complex jobs easier to manage. Working with a machine shop Houston supplier should function like bringing in an engineering partner and not simply placing a purchase order.

Machine Shop Houston Project Cost, Lead Time, And Scalability

Knowing the cost drivers and lead-time factors is essential for engineers and purchasing teams. These factors depend on materials, geometry, tolerance, and finish requirements. Accurate specifications are necessary for clear supplier estimates.

Factors Affecting Price And Timing

The selected alloy or plastic strongly affects both cost and machining time. As one example, aluminum usually cuts more quickly than stainless, which can make stainless jobs slower and harder on tooling. Intricate shapes and deep internal features also increase production duration. Additional finishing steps like cryogenic deburring, anodizing, or coatings add days to lead time and add handling expense.

Volume significantly affects pricing. A single prototype absorbs front-end CAM and fixture costs. On the other hand, repeat batches distribute those costs over many parts. Larger production work supports purpose-built fixtures and dedicated tools, reducing cycle time. Accurate CAD/CAM files with clear tolerances help suppliers quote correctly and help suppliers commit faster.

How Scaling From Prototype To Production Works

Moving machining from prototype to volume depends on controlled equipment, fixtures, and inspection steps. Providers like Lowrance Machine invest in multi-axis equipment and high-capacity milling platforms. That equipment base supports quality during production ramp-up, lowering risk in scaling from first articles to repeat manufacturing.

Practical savings methods include live-tool machining, better toolpaths, and purpose-built fixtures. That approach decrease transfers and machining duration per component. Choosing alloys and finishing processes that reduce secondary steps can lower total cost. CNC milling in Houston, when used strategically, can remove some follow-up work by consolidating operations into fewer setups.

Supplier quoting and schedule commitments depend on precise information. Supply accurate CAD and CAM data, detailed tolerances, and acceptance of suggested process optimizations. Good communication with a shop reduces back-and-forth, leading to more reliable pricing and scheduling.

Driver Effect On Price Impact On Lead Time Mitigation
Material choice, such as aluminum vs stainless Aluminum is usually cheaper to machine; stainless may raise tool and run costs Stainless can lengthen cycle time Choose alloy with similar properties that machines easier
Component complexity and features More complex raises programming and run cost Complex features can add production time Apply multi-axis CNC Milling Houston to reduce setups
Dimensional tolerances and finish Strict specifications increase QA and machining cost High-precision jobs often need slower cutting and more inspection Match tolerance to function and avoid unnecessary fine finishes
Volume Larger runs reduce unit cost by spreading tooling expense Production lots add planning time but improve per-part throughput Plan runs to benefit from tooling amortization
Secondary processes Heat treat and plating can add outside-vendor costs Every outside process can add queue and transit time Choose materials and finishes that minimize extra steps
CAM and fixture optimization Optimized CAM and workholding lower unit cost Refined setups reduce total production time Use machining services Houston expertise to improve CAM and fixturing

Conclusion

Houston’s industrial manufacturing base is perfect for CNC Milling Houston projects needing accuracy and quick turnaround. Local shops use high-capability machinery from brands like DMG MORI and Okuma. Many also provide live tooling, long-bed turning, EDM, and internal finishing. This setup makes possible quick movement from prototype to production.

When picking a CNC machine shop Houston, review specifications, expected quantities, and inspection requirements. Ask about certifications like ISO 9001 or AS9100D. Detailed quotes and honest schedule estimates are important for preventing delays. They ensure the chosen shop can grow with your needs.

For machining services Houston that include secondary finishing plus assembly help, assess end-to-end capabilities and communication. The Lowrance Machine team supports the complete path from first article through repeat production. Its staff can provide technical reviews and quotation support to support your dimensional needs and schedule goals.

Related: Customer Service Skills of Houston Unarmed Security Guards

Explore Precision CNC Machining Solutions

High-Precision Manufacturing With CNC transforms parts from early prototype stages into production with extreme precision. Well-known shops such as Leech Industries and High Tech Quality Manufacturing exemplify the practical synergy created by advanced CNC machining services. They rely on 5-axis mills, Swiss machines, wire EDM, and stringent quality systems to achieve precise tolerances.

High-Precision Manufacturing With CNC And Traditional Machining Methods
Precision CNC machining is valued by manufacturers because it reduces variability, cuts rework, and strengthens customer satisfaction. Current capabilities often include high-speed spindles reaching 20,000 RPM, large tool magazines, multi-axis control up to nine axes, and accuracy in the +/- .0002″ range.

When U.S. clients need reliable CNC machining solutions, Lowrance Machine stands as a trusted partner. Its operations adhere to industry benchmarks with quick CNC prototyping, ISO-compliant quality systems, and the capacity to take on both single prototypes and major production volumes.

Important Takeaways

  • High-Precision Manufacturing With CNC ties prototyping with scalable production while leveraging advanced machine tools.
  • Complete CNC machining services include milling, turning, 5-axis, Swiss, and EDM operations.
  • By producing consistent, tight tolerances, precision CNC machining strengthens yield and customer confidence.
  • Today’s CNC machining solutions make possible hard milling, high spindle speeds, and large work envelopes.
  • Lowrance Machine serves as a qualified U.S. partner that is skilled at executing high-precision projects to industry standards.

Introduction To High-Precision Manufacturing With CNC

High-precision manufacturing with CNC integrates advanced machine tools, strict process control, and modern CAD/CAM systems. That synergy allows parts to move quickly from concept to consistent production while meeting demanding tolerances and traceability standards.

Defining High-Precision Manufacturing And CNC Integration

The focus of high-precision manufacturing is consistent results, superior surface finish, and precise dimensional control. Using milling, turning, and multi-axis strategies, CNC machining can hold tolerances as close as +/- .0002″. CAD/CAM programmers generate validated toolpaths that allow machines from Haas, DMG MORI, and Mazak to hold consistent outcomes.

Why CNC Precision Matters Across Major Industries

Precise fits are critical in aerospace because both safety and performance depend on them. Medical implants require traceable processes and ISO 13485 compliance to support patient safety. Automotive systems rely on consistent geometry for durability, while electronics require exact form factors to preserve signal integrity. In each of these industries, CNC precision engineering reduces risk and supports certification.

Lowrance Machine CNC And Manual Machining Services

How CNC Lowers Variability And Improves Customer Satisfaction

With computer control, repeatable toolpaths, and automatic tool changes, human error is cut significantly. Rapid CNC prototyping helps test CAD models ahead of production and thereby reduces rework. Techniques such as CMM inspection and statistical process control reinforce consistency. That consistency builds customer confidence and brand trust.

These same methods are followed by Lowrance Machine to limit variability and satisfy industry standards. A commitment to high-accuracy manufacturing, finishing work, and traceable marking supports the delivery of dependable components for aerospace, medical, automotive, and electronics sectors.

Capabilities In CNC Machining Services

Lowrance Machine offers a broad range of CNC machining services, from simple prototypes to complex production runs. Conventional milling and turning are combined with advanced machining cells so the company can serve aerospace, medical, and industrial markets. That combination makes it easier for customers to identify CNC machining solutions that support their precise requirements.

CNC milling, turning, drilling, and boring are all part of the available service mix. By using 5-axis machining, shops can approach intricate work from several angles in one setup. Cycle efficiency is raised by high-speed spindles reaching 20,000 RPM and tool magazines that may hold up to 80 tools.

More difficult work becomes possible through advanced machining methods. With multi-axis machining and 3-D high-speed milling, complex contours can be produced rapidly. Swiss machining works especially well for small, detailed cylindrical parts commonly used in medical devices. Shops also use wire EDM and laser marking for precise detail and traceability, and they complete projects with finishing work such as heat treating, welding, and assembly.

Machine size is critical when determining what part scope a facility can support. In many shops, milling capacity reaches roughly 30″ x 65″, and turning centers can accommodate parts up to 26″ in diameter and 80″ long. When machines offer as many as nine axes, simultaneous motions become possible and setup counts drop in high-mix, low-volume production.

Respected builders like Mazak, Okuma, Kitamura, Grob, Haas, DMG Mori, Doosan, and Hurco are frequently found in advanced machining cells. The right machine choice is essential when precision CNC machining and repeatable results are the goal.

Lowrance Machine strives to match that level of capability and service. By combining experienced programmers, advanced inspection equipment, and flexible machine layouts, the shop offers CNC machining solutions that lower lead times and limit costs. Clients gain the benefit of streamlined workflows and single-source accountability on complex parts.

It is wise to ask a provider about spindle specs, tool capacity, axis counts, and examples of similar parts produced. These details help confirm whether the shop can meet the tolerance and surface-finish requirements associated with high-precision work and multi-axis machining.

Materials Used In High-Accuracy Manufacturing

Every component in high-accuracy manufacturing depends on selecting the proper material and process. Material selection affects tooling, spindle speed, cutting fluid, fixturing, heat treatment, and inspection strategy. Makers such as Mazak and Haas offer capability references across a broad range of alloys and medical-grade plastics, providing useful guidance in both prototype and production phases.

Machined materials commonly fall into major families as well as a number of specialized categories. Below is a table that helps engineers connect material choice with manufacturing strategy by outlining machinability notes, finishing methods, and common uses.

Material Family Examples Important Machining Notes Representative Applications
Aluminum And Copper Alloys 6061-T6, 7075, C11000, brass High removal rates with fine surface finish; coated tools extend life; burrs must be monitored on thin walls Lightweight components, aerospace housings, electrical connectors
Alloy And Stainless Steels 304/316, alloy steels, 17-4 PH Rigid fixturing is needed; heat buildup must be controlled; passivation and heat treat are common options Fasteners, medical instruments, structural components
Nickel And Titanium Alloys Ti-6Al-4V, Inconel 718, Hastelloy Low thermal conductivity and work hardening call for slower feeds and robust tooling Exhaust systems, engine components, and high-temperature applications
Tool Steels And Hardened Alloys A2, H13, D2, 9Ni-4Co-0.30C Usually roughed prior to heat treatment and finished later; EDM or grinding may support tight features Molds, dies, and wear components
Exotic And Specialty Materials Copper tungsten, carbide, Vespel, beryllium copper Special cutting strategies are needed, and both coolant and tool geometry are critical to accuracy Vacuum components, insulating parts, high-performance electrical contacts
Ceramics & Graphite Alumina, silicon carbide, machinable graphite Because of brittle behavior, cutting must stay slow and controlled, and diamond tooling is often preferred Semiconductor tooling, thermal components, electrodes
Composite And Plastic Materials UHMW, PEEK, PTFE, medical-grade polymers, carbon fiber laminates Reduced speeds and strong chip evacuation are needed because of low melting points; composite delamination must be controlled Insulators, implant supports, lightweight structural parts

Specifying exotic materials should trigger early conversations with the machine shop about limits and post-process requirements. The importance of clearly defined tolerance and finish requirements is highlighted by Lowrance Machine so tooling, cutting fluids, and secondary processes can be planned effectively. Clear specifications lead to stronger process planning and easier compliance with regulatory demands.

Precision CNC machining of difficult alloys affects setup times and cycle planning. In the prototyping stage, engineers benefit from testing candidate materials to verify dimensional stability after secondary operations. This reduces the chance of surprises later when the job moves into scaled high-accuracy manufacturing.

To specify parts properly, it is important to state the exact alloy or polymer grade, the desired tolerance range, and any certification requirements. That level of detail lets shops optimize toolpaths, fixturing, and inspection plans. That makes it more likely the machined material will meet performance expectations without unnecessary rework.

Precision CNC Machining Quality And Tolerance Standards

Clear quality and tolerance benchmarks are essential when repeatable parts are the goal. Specialized shops in precision CNC machining typically explain repeatability levels, setup methods, and machine features that support stability. Large tool carousels, pallet changers, and correctly sized machines help reduce fixture changes and limit holding-pressure variation.

Achievable Repeatability And Tolerance Levels

Modern machines can maintain very close tolerances when the platform is stable and setup demands are minimized. It is possible to achieve repeatability down to +/- 0.0002″ on stable systems under the right conditions. Actual tolerance depends on the material and operation, though milling and turning often keep critical features within a few ten-thousandths.

Quality Control And Inspection

CMM inspection provides dimensional traceability and full reporting options for customers. Statistical process control charts monitor drift and tool wear across repeated runs. Before shipment, visual checks and functional tests help confirm fit and finish. To validate each batch, experienced CNC machining specialists commonly provide CMM plots, inspection reports, and SPC data.

Regulatory And Certification Considerations

Medical and aerospace work demands documented systems and proven compliance. Common certifications include ISO 9001:2015, AS9100D for aerospace, and ISO 13485 for medical devices. NIST calibration, ITAR controls where applicable, and documented passivation or finishing steps support durability and regulatory acceptance.

It is important for Lowrance Machine and similar professional shops to spell out achievable tolerances, provide inspection proof, and disclose certifications at the start. Such openness makes it easier for engineers to choose the right partner for high-tolerance CNC manufacturing and keep expectations realistic.

CNC Precision Engineering From CAD To Production

Taking a part from CAD model to dependable production demands a sequence of disciplined steps and strict process control. By aligning prototyping, validation, and production, CNC precision engineering helps designers and manufacturers reach specifications faster while generating less waste.

Model verification is accelerated by Rapid CNC prototyping. Using CAD/CAM validation, additive support, and wire EDM when needed, shops can confirm fit, form, and function quickly. This early phase reveals geometry issues before final tooling and fixturing are committed.

Using one-and-done machining strategies can sharply reduce setup requirements. Modern equipment with large tool carousels, pallet changers, and automatic part loaders allows complex parts to be completed in a single operation. The benefit is improved dimensional stability and fewer handling errors on high-precision parts.

One-and-done machining is often strengthened by cellular manufacturing. By grouping machines, fixtures, and personnel into coordinated units, it improves the flow from prototype refinement to low-volume production. Process documentation and CAM verification help every cell produce parts within required tolerances on a repeatable basis.

Urgent low-volume demands are supported through quick-turn solutions. Shops that deliver prototype and short-run parts fast while maintaining inspection records provide a major advantage. Flexible scheduling, tool readiness, and clear CAD/CAM data from the outset are key to successful quick-turn work.

At Lowrance Machine, CAD/CAM verification, prototype validation, one-and-done machining, and cellular manufacturing are brought together in one workflow. The result is shorter lead times and stronger confidence that the next builds will match the intended specification.

High-Tolerance CNC Manufacturing For Complex Geometries

Complex shapes combined with strict tolerances demand advanced machines and disciplined planning. Distortion is controlled and consistency is maintained in high-tolerance CNC manufacturing through multi-axis capability and documented fixturing.

Using 5-Axis And Multi-Axis Machining For Complex Shapes

With five-axis machining, teams can access contoured surfaces in a single operation and thereby lower cycle time and error. When this is paired with machines offering up to nine axes, 3-D high-speed machining becomes possible and form tolerances remain tight.

Benefits Of Using The Right-Sized Machine For Holding Pressure And Dimensional Stability

Selecting a machine that matches the part size and clamping strategy helps reduce deformation during cutting. With properly sized equipment, holding pressure stays more controlled, and that matters greatly for repeatability in high-accuracy manufacturing. It is especially important in jobs where tolerances around +/- .0002″ must be maintained.

High-Tolerance Applications In Aerospace, Medical, And Precision Dies

Applications such as aerospace fittings, implantable medical devices, and precision dies demand both intricate geometry and exact fit. Manufacturers often combine 5-axis machining, Swiss turning, and wire EDM to create precision components that meet these demands.

To maintain consistency from prototype to production, Lowrance Machine and similar suppliers document fixturing, program flow, and inspection points. That documentation improves traceability and lowers the risk of rework on critical parts.

Choosing CNC Machining Specialists And Evaluating Facilities

The search for a precision-work partner should begin with a detailed review of the machine shop. Rather than relying on broad marketing claims, it is important to confirm that advanced equipment from respected brands such as Mazak, Okuma, Kitamura, and Grob is actually present. Just as important is the shop’s ability to repeat results on similar work.

Capability statements, previous production examples, and detailed documentation of prototyping and validation should all be requested. That step helps separate genuinely capable shops from operations that only sound impressive in promotion.

Personnel quality matters as much as equipment quality. It is important to ask about staff experience, certifications, and proven work in sectors such as aerospace, medical, and defense. Where applicable, standards such as AS9100D, ISO 9001, and traceability tied to NIST or ITAR need to be confirmed.

For varied workloads, cellular manufacturing is often the most efficient production model. This approach lowers idle time, helps extend tool life, and makes setup work easier to manage. Features such as large tool magazines, pallet changers, part loaders, and bar feeders usually indicate stronger production readiness and consistency.

Quality-focused shops rely on structured inspection and statistical process control systems. Buyers should ask to see CMM reports, sampling plans, and proof that SPC is used in production. Prototyping and first-article inspection should also be standard parts of the workflow. This is one of the clearest differences between highly experienced CNC machining specialists and weaker competitors.

When evaluating a partner, use a concise checklist that covers certifications, CMM and SPC methods, equipment inventory, machine-brand specifics, and maintenance records. Buyers should ask for evidence of quick-turn performance and clear plans for scaling production as well. When asked, suppliers like Lowrance Machine should be ready to share documentation and case studies.

An ideal partner is one that balances strong machines, experienced personnel, and efficient workflow design. Facilities showing real strength in cellular manufacturing, automation, and similar prior work should rise to the top. By reviewing a partner thoroughly, teams reduce project risk and improve the odds of meeting both schedule and tolerance targets.

How High-Precision Manufacturing With CNC Improves Product Quality

Field performance can be transformed by high-precision production. Failure risk drops and customer confidence grows when tight tolerances are maintained. That shows up as fewer returns, more consistent performance, and a stronger brand reputation.

How Precision Machining Drives Customer Satisfaction And Brand Trust

Product consistency begins with part consistency. By minimizing variation, precision CNC machining helps final assemblies meet specification every time. As reliability increases, customer satisfaction improves and repeat business becomes more likely.

Research indicates that 63% of consumers would pay more when quality is higher. Precision investment by companies such as Lowrance Machine can protect brand reputation and support long-term customer loyalty.

The Cost-Benefit Of Precision CNC Work

Stable machines and advanced setups reduce setup time and rework. Processes such as one-and-done machining and cellular manufacturing help boost yields and shorten lead times.

Lower rework creates clear savings across production and warranty budgets. New products can reach the market more quickly when scrap and corrective work are reduced.

Cases Where Precision Wins Over Lower-Cost Alternatives

For medical implants and aerospace flight hardware, precision is a requirement rather than a luxury. Dependable finishing and inspection on high-precision parts help prevent recalls and regulatory penalties.

Even when the upfront machining cost is higher, the long-term savings from fewer returns, reduced warranty claims, and less regulatory risk can make the investment worthwhile. Selecting precision CNC machining is a strategic decision that supports durable performance and measurable life-cycle savings.

Where CNC Machining Solutions Deliver Real-World Value

Real-world production challenges are addressed by advanced shops through precision technology. Many CNC machining solutions are used for parts that face harsh conditions, strict certification demands, and tight tolerance requirements. Below are examples that illustrate how machining technology is matched to sector-specific needs.

Aerospace Use Cases

Repeatable accuracy and fatigue-resistant finishes are essential for airframe fittings, engine brackets, and flight-control components. To satisfy AS9100D and ITAR requirements, aerospace machining often relies on high spindle speeds, hard milling, and large work envelopes. Lowrance Machine and similar suppliers use 5-axis centers to support prototype runs and production quantities in titanium and Inconel.

Medical Use Cases

Medical CNC machining produces implants, surgical tools, and diagnostic housings. To support patient safety, shops working to ISO 13485 maintain traceability, sterile-compatible finishes, and strict tolerances. Swiss machining and wire EDM are common choices where tiny features and burr-free edges are critical.

Automotive And Defense

Engine, transmission, and chassis parts require consistent interchangeability in automotive production. In defense work, mission-critical parts require rugged materials and thoroughly documented processes for field reliability. Both sectors also rely on quick prototyping to verify designs before moving to larger production volumes.

Semiconductor And Electronics Examples

Connectors, housings, and wafer-processing tooling require micron-level accuracy and machining practices compatible with cleanroom environments. Specialized fixturing and laser marking are commonly used in semiconductor component work to satisfy thermal and traceability requirements.

Oil, Gas, And Industrial Wear-Part Applications

In oil, gas, and industrial wear applications, valves, seats, and pump parts often operate under abrasive and erosive conditions. Hardened surfaces and tight clearances created through CNC machining solutions can significantly improve service life. Alloy steels and tungsten-carbide composites are commonly selected for wear resistance.

Cross-Industry Capabilities

  • Prototyping verifies fit and function ahead of production, reducing the need for late-stage changes.
  • Process controls and certifications support regulated sectors such as aerospace and medical CNC machining.
  • Specialized workflows such as Swiss, 5-axis, EDM, and laser marking adapt well to diverse industry needs.

Conclusion

Advanced machining methods, extensive material options, and demanding inspection systems all come together in High-Precision Manufacturing With CNC. That combination produces parts that meet strict dimensional and functional requirements. With 5-axis and multi-axis machining, Swiss turning, wire EDM, high-speed spindles, and large tool magazines, shops can often reach precision near ±0.0002″. Such technology and process discipline form the backbone of CNC precision engineering across aerospace, medical, automotive, and electronics sectors.

Through quality systems such as CMM inspection, statistical process control, and certifications like AS9100D, ISO 13485, and ISO 9001, parts can be validated against regulatory and customer requirements. As a result, rework is reduced, yields improve, and time-to-market becomes shorter. When rapid development is needed, quick-turn prototyping and validated CAD/CAM workflows reduce risk while easing the shift from prototype to production.

U.S. manufacturers seeking reliable outcomes often benefit from partnering with experienced CNC machining specialists. Those specialists combine scalable setups, cellular manufacturing, one-and-done machining, and strict quality practices. When used well, high-tolerance CNC manufacturing can reduce downstream cost while improving performance in demanding applications.

By embracing these established methods, teams put themselves in a stronger position to succeed in both precision and delivery. When performance, traceability, and speed matter most, CNC precision engineering and disciplined manufacturing processes create meaningful technical and business advantages.

Related: The Bar Feeding in CNC Lathe Machining in Dallas

Stranding Efficiency Metrics for an SZ Stranding Line

Could the machines building fiber optic cable production machinery be the unseen force that finally brings true gigabit access to every American home? This article explores the recent breakthroughs in FTTH Cable Production Line Technology. These advancements are reshaping broadband network infrastructure and speeding up fiber to the home technology across the United States.

SZ Stranding Line

FTTH Cable Production Line

Fiber Draw Tower

Modern advancements in automation, precision engineering, and AI-driven inspection are greatly cutting production costs and boosting quality. This synergy makes high-speed internet technology more dependable and simpler to deploy for service providers and municipalities.

Global optical cable output now exceeds hundreds of millions of kilometers annually. This surge is fueled by 5G deployments, hyperscale data centers, and the growing demand for streaming and remote work. The subsequent sections will cover automation and Industry 4.0, the use of low-loss materials, AI quality control, innovative cable designs such as bend-insensitive fiber and flat drop microcables, and the pursuit of sustainability in production lines.

Telecommunications manufacturing, network planning, and procurement professionals will discover valuable insights. These insights focus on selecting the right fiber optic cable production machinery and optimizing processes. They are designed to meet regional deployment needs and future bandwidth growth.

FTTH Cable Production Line Technology

The term encompasses the machinery, control systems, and materials transforming optical preforms into deployable fiber cables. It includes fiber drawing and coating, SZ stranding, ribbon formation, extrusion of jackets, armoring, taping, automated testing, and final take-up systems. Each step’s precise control defines the fiber optic cable production process, ensuring consistent performance.

The manufacturing chain demands stringent tolerances. SZ stranding systems align dozens of strands with micron-level tension precision. Extrusion lines employ servo-driven extruders and laser micrometers to maintain jacket thickness within ±0.02 mm. Such precision minimizes variability, lowering attenuation and making field splicing easier.

Standards and regulatory frameworks heavily affect manufacturing decisions. Compliance with ITU-T recommendations, such as G.657, and regional fire codes like CPR in Europe, is essential. Meeting these standards ensures products align with the broader broadband network infrastructure.

Quality in production directly impacts network economics and service delivery. Lower attenuation and consistent geometry reduce splice loss and extend reach. This enhances reliability for carriers, ISPs, and utilities, while lowering the total cost of ownership for FTTH deployments. The growing demand for symmetrical multi-gigabit services, 5G backhaul, and data center interconnect is driving the scale-up of modern lines.

Comparing key process components and tolerances reveals their impact on output and quality.

SZ Stranding Line

Production Component Typical Parameter Control Impact on Performance
Fiber drawing & coating ±1°C temperature control; coating concentricity ±5 µm Consistent geometry; reduced macrobend loss
Ribbon formation and SZ stranding Tension control at micron scale; synchronization to 0.5 ms Uniform fiber pitch; predictable splice and connector performance
Extrusion & jacket thickness Laser-based feedback; ±0.02 mm thickness control Consistent mechanical protection; predictable installation behavior
Tape wrapping and armoring Servo feed rate; layer alignment control Improved crush resistance; compliant aerial/underground specs
Automated testing and take-up OTDR and insertion-loss verification at production speed; controlled winding tension 100% traceable quality; reduced rework and field failures

Manufacturers like Corning, Prysmian Group, and Sumitomo Electric focus on tighter process control to meet operator expectations. Continuous advancements in the fiber optic cable production process enable networks to scale while maintaining performance in the last mile of broadband network infrastructure.

Automation And Industry 4.0 In Fiber Optic Cable Production

Factory floors for fiber optic cable production machinery now mirror advanced manufacturing plants from other industries. Smart controls, synchronized stages, and data-driven decision making raise output and protect quality. These shifts shorten commissioning time for new product families. They let telecommunications equipment manufacturers pivot between armored aerial lines and microcable runs with minimal downtime.

Smart machinery and PLC coordination

Programmable logic controllers coordinate stranding frames, ribbon formers, and take-up units to keep tension within sub-0.01mm windows. Servo-driven extrusion coupled with laser micrometers enforce ±0.02mm jacket thickness. The result is fewer rejects, less rework, and consistent optical performance on every reel.

Edge computing and process orchestration

Local edge servers ingest terabytes of telemetry each day. They drive low-latency closed-loop adjustments and push immediate alerts when deviations occur. This approach keeps optical fiber cable equipment running at peak efficiency. It supports real-time quality assurance during long production runs.

AGVs, material handling, and workflow gains

Automated Guided Vehicles move heavy cable drums with millimeter-level repeatability. Laser-navigated AGVs reduce manual handling injuries and speed material flow between extrusion, curing, and drum stations. This automation lowers labor costs while raising throughput on ftth cable production line technology setups.

Benefits for makers and the supply chain

  • Greater throughput with repeatable outcomes
  • Accelerated prototyping and reduced time to market
  • Reduced labor exposure and lower operating cost
  • Stronger connectivity between optical fiber cable equipment and enterprise platforms

Industry ecosystem and adoption

Leading telecommunications equipment manufacturers pair PLCs with robotic arms, AGVs, and industrial IoT stacks to reach Industry 4.0 goals. This integration creates a resilient production base. It is able to adapt as demand shifts toward denser, more complex FTTH offerings.

Precision Engineering Breakthroughs For Lower Attenuation

Advances in materials and mechanical design are driving down loss in modern fiber lines. Engineers pair ultra-low loss fiber with tighter coating control to reduce intrinsic and bending attenuation. These gains matter to network operators who want longer spans and fewer amplifiers in high-speed internet technology deployments.

The fiber optic cable production process now favors smaller coated diameters such as 180µm and 160µm. These sizes let manufacturers increase fiber count and build denser microcables without sacrificing handling or optical stability.

Low-Loss Glass And Advanced Coatings

Manufacturers use improved glass formulations that lower Rayleigh scattering and reduce baseline attenuation. Ultra-low loss fiber variants extend reach for long-haul and high-capacity links while easing repeaters and amplifier requirements.

Coating chemistry has progressed too. UV-cured acrylate systems cut microbending loss by roughly 40% compared with earlier generations. That performance drop helps maintain signal integrity in cramped ducts and tight bends common in FTTH and 5G backhaul networks.

Central Strength Members And Mechanical Design

Mechanical design updates center on robustness and dimensional control. Fiber-reinforced plastic (FRP) rods with tensile strengths near 1.2 GPa serve as central strength members. They limit elongation during pulling and boost crush and bending resilience.

Water-blocking advances use swellable yarns and grease-free gel compounds to achieve near-complete moisture resistance. These measures protect optical paths and raise in-service reliability for cable installations in challenging environments.

These precision engineering steps integrate directly into fiber optic cable manufacturing workflows. When the production line aligns glass, coating, and mechanical specs, attenuation falls and networks gain reliability. That alignment shortens time to service for operators deploying modern broadband and high-speed internet technology.

Quality Control 4.0 And AI-Powered Inspection

Smart factories for fiber optic cable production now embed inspection systems that run continuously. These systems combine machine vision, machine learning, and automated testers to watch every reel and spool. The result is tighter feedback during the fiber optic cable production process and fewer surprises in the field.

AI models score coating uniformity, microbends, and surface defects at line speed. They cross-reference process telemetry from fiber optic cable production machinery and predict deviations hours before a reel moves to final spooling. This allows for in-line adjustments without stopping the line.

Automated OTDR integration performs 100% attenuation testing on every length. Modern OTDR systems using 1550nm sources map loss across reels and flag changes as small as 0.01 dB/km. Inline OTDR logs feed edge analytics for rapid root-cause tracing when a batch shows anomalies.

Robotic bend-radius simulators apply repeated stress cycles while monitoring macrobend loss. These testers validate compliance with ITU-T G.657 and customer bend specifications by running controlled bends at multiples of the cable diameter. Test outcomes are tied to batch IDs for traceability.

Thermal cycling chambers stress jackets and splices across wide temperature ranges. Environmental tests up to +85°C and down to -60°C confirm stability for extreme climates. Automated logs record each chamber run and link results to production lots.

Quality control 4.0 reduces returns and field failures by making 100% in-line testing routine. Edge analytics and OTDR integration shorten diagnosis times and improve regulatory compliance. Broadband operators see fewer truck rolls and better lifecycle performance for FTTH networks.

Cable Design Innovations For FTTH Deployments

New cable designs address common field challenges in fiber to the home technology. Engineers focus on durability, space economy, and speed of activation. These trends reduce installation time and lower long-term operational costs.

Bend-Insensitive Fiber Benefits For MDUs And Tight Routing

Bend-insensitive fiber maintains signal strength when routed around corners and through confined spaces. ITU-T G.657 compliant fibers minimize attenuation at tight radii, protecting links in multi-dwelling units and behind baseboards. Prysmian’s BendBright family and BendBrightXS exemplify how smaller coated diameters facilitate routing without compromising optical performance.

Flat Drop And Microcable Options For Flexible Deployments

Flat drop cable remains a preferred choice for aerial self-support, duct installs, and direct burial in North America. Its profile accommodates narrow pathways and enhances aerial spans with appropriate clamps. High-fiber-count flat drops necessitate enhanced radial strength and more robust hardware for longer spans.

Microcable technologies reduce outside plant profiles to 8 mm or less. Microcables and air-blown systems enable capacity addition inside existing ducts and congested corridors. These approaches reduce civil works, lower labor costs, and facilitate incremental network growth for urban and campus builds.

Pre-Connectorized Solutions To Speed Field Activation

Pre-connectorized solutions offer factory-terminated, plug-and-play assemblies that minimize field fusion and connector errors. Hardened outdoor connectors and vendor offerings like Prysmian’s ezDROP simplify mass rollouts and enhance first-pass yield. Service teams experience fewer truck rolls and faster service turn-up for smart city and 5G edge projects.

Design Type Core Advantage Typical Application Key Deployment Consideration
Bend-insensitive optical fiber Reliable performance at tight radii Multi-dwelling units, indoor routing, compact pathways Choose ITU-T G.657 variants for indoor runs
Flat drop fiber cable Multiple deployment modes Aerial drops, direct burial, duct insertion Use proper clamps and radial-strength hardware
Microcable solutions Compact profile with scalable capacity Microduct installs, congested urban ducts Compatible blower tools are required for air-blown systems
Pre-terminated solutions Faster field activation and fewer errors Large deployments, rapid activation Prepare for standardized connector interfaces

Sustainability And Energy Efficiency In Production Lines

Manufacturers in the fiber optic cable industry are embracing greener practices to reduce costs and meet consumer demands. Facilities prioritizing sustainable production witness improvements in operational efficiency and brand reputation. These advancements impact power systems, cooling, raw materials, and waste management.

Recovered energy systems strategies are becoming prevalent on extrusion lines and take-up reels. Regenerative braking on motor-driven spools returns power to the grid, thereby lowering net consumption. Studies indicate that energy recovery can reduce drive energy use by up to 32 percent in retrofitted reels.

Closed-loop cooling and chiller-less extrusion systems are reducing water demand. Adiabatic cooling can decrease water use by as much as 75 percent, particularly beneficial in water-scarce areas. Plants employing closed-loop cooling systems, in conjunction with heat exchangers, maintain temperature control while reducing utility expenses.

Recyclable jacket materials are transforming the disposal of cables. New polypropylene-based and modified polymer compounds meet mechanical and fire-safety standards, enabling higher recycling rates. Suppliers like Borealis and LyondellBasell are developing compounds that support the circular economy in cable jackets.

Process optimization minimizes scrap before recycling. Precision extrusion, in-line laser measurement, and real-time analytics reduce off-spec runs. Digital twins enable engineers to refine parameters, enhancing batch yields and reducing material waste.

Regulatory pressures and corporate ESG goals are compelling operators to favor vendors with transparent sustainability metrics. Municipal procurement teams and large network operators increasingly consider lifecycle impacts when selecting suppliers.

Operational Area Typical Improvement Main Benefit
Regenerative drives on take-up reels As much as 32% lower energy use Lower electricity costs and reduced peak demand
Adiabatic and closed-loop cooling systems Approximately 75% reduction in water use Lower water expenses and better compliance in arid areas
Recyclable cable jacket materials Greater post-consumer recyclability Better circularity and simpler end-of-life handling
Inline inspection and digital twins Scrap and off-spec runs cut by double digits Better yield, less material waste
Reporting and sustainability certifications Better standing in procurement Competitive advantage with network operators

Implementing these measures enhances the resilience of fiber optic cable manufacturing. It leads to lower lifecycle costs and easier compliance. Manufacturers integrating energy recovery and recyclable jacket materials position themselves for growth in the green procurement market.

Emerging Technologies Shaping Cable Manufacturing

New technologies are transforming the design and operation of fiber optic cable production machinery. These innovations expedite commissioning, diminish prototyping cycles, and empower manufacturers to test process alterations without halting production.

Digital twins create virtual replicas of entire production lines and novel cable designs. Engineers at Corning and Prysmian leverage these models to validate footprint, material flow, and layout before physical construction. Studies indicate commissioning can be up to 60% swifter when teams execute virtual scenarios and optimize layouts beforehand.

Digital twins facilitate expedited R&D for bespoke items such as armored variants and anti-rodent jackets. Virtual testing minimizes the necessity for physical prototypes and accelerates market entry. Teams can simulate process modifications, observe material interactions, and refine equipment parameters in a risk-free milieu.

AI systems introduce predictive capabilities on the factory floor. Machine learning scrutinizes 50+ parameters to forecast failures and quality deviations hours in advance. This AI predictive maintenance lessens unplanned downtime and elevates overall equipment effectiveness for high-volume lines.

Manufacturers like Siemens and ABB integrate AI with edge computing, enabling models to operate proximal to machines. Alerts prompt targeted inspections, spare part staging, and corrective actions before a fault halts production. This strategy maintains yield and shortens mean time to repair.

Quantum fiber sensing and distributed monitoring extend capabilities beyond production to the deployed cable. Embedded Brillouin and distributed acoustic sensing provide continuous strain and temperature data across extensive spans.

Integration of quantum fiber sensing enhances network diagnostics and supports structural health monitoring. Field teams acquire actionable insights when sensing data is linked to manufacturing records and test logs. This connection enables tracing anomalies to specific production batches.

Combined workflows—digital twins plus AI predictive maintenance—accelerate both commissioning and product development. Manufacturers embracing these tools can respond more swiftly to market fluctuations and deliver higher-value, differentiated cables.

Market-Driven Production Adaptations And Regional Needs

The global demand for fiber access compels manufacturers to adapt their production lines to local requirements. Regional fiber optic cable manufacturing now emphasizes durability, density, and safety. Plants employ modular equipment, enabling swift transitions between product families and meeting specific operator needs without significant delays.

In North America, networks predominantly opt for aerial routes and robust outside-plant solutions. Producers concentrate on creating armored aerial cables with enhanced breaking strength, corrosion-resistant armor, and simplified pole-mount installation. These designs withstand wind, ice, and long span stresses typical of utility corridors.

North American Priorities: Aerial And Armored Designs

Armored aerial cables are engineered for enduring reliability on poles and open spans. They boast 1,200 lb or greater tensile ratings and integrated steel or aluminum armoring to safeguard fibers against mechanical damage. Manufacturers deploy modular armoring units and rapid testing rigs, enabling mass production of these variants.

APAC And Europe: High-Density Microcables And Regulatory Compliance

In APAC, the scarcity of space and the need for dense builds drive demand for high-density microcables. These cables feature compact stranding towers and reduced-diameter fiber stacks, allowing for more fibers per duct. They significantly reduce civil costs by facilitating quicker overbuilds and easier microtrenching.

Europe mandates strict regulatory compliance for buildings and public spaces. Producers offer halogen-free, flame-retardant jackets that meet CPR classes like B2ca. Compliance testing is integrated into production lines, ensuring products meet fire-safety rules for indoor and outdoor applications promptly.

Across regions, the ability to adapt production is paramount. Compact stranding towers, modular extrusion and armoring units, and rapid prototyping enable factories to switch from armored aerial cables to microcable runs in mere hours. This flexibility allows operators to fulfill unique specifications while adhering to local codes.

Case Studies And Manufacturer Spotlight: Shanghai Weiye OFC Equipment

Shanghai Weiye OFC Equipment has solidified its reputation as a leading telecommunications equipment manufacturer. They cater to the FTTH and broader fiber markets. Their optical fiber cable equipment boasts advanced features, including SZ stranding, ribbon production, and extrusion with servo control. This ensures tight tolerances and high yields.

Their machinery for fiber optic cable production is equally impressive. It includes tape armoring units, automated take-up reels with regenerative drives, and integrated OTDR and vision inspection stations. These systems support various applications, such as bend-insensitive fiber, microcables, and pre-connectorized solutions. These are crucial for FTTH, 5G backhaul, and dense urban deployments.

Quality and sustainability are integral to their offerings. They employ OTDR testing, AI-powered inspection, and robotic bend simulators to meet QC 4.0 standards. Additionally, energy recovery options and closed-loop cooling reduce operating costs and scrap. Modular designs with AGV and edge computing support enable rapid reconfiguration and digital twin commissioning, catering to U.S. manufacturers and contract producers.

For operators in the United States, investing in Shanghai Weiye OFC Equipment can significantly enhance production capabilities. It ensures compliance with strict attenuation and mechanical specifications. This accelerates the introduction of new cable families, vital for broadband expansion. The company’s systems harmonize technical performance with practical manufacturing requirements.

FAQ

Q: What Advances Define Modern FTTH Cable Production Line Technology?

A: Modern FTTH cable production lines integrate high-precision mechanical systems with servo-driven extrusion. They utilize SZ stranding and ribbon machines, along with automated take-up reels. These systems also include integrated OTDR and AI-driven vision inspection, PLC orchestration, AGV material handling, and edge computing. Such advancements enable micron-level tension control and ±0.02mm jacket thickness tolerances. They achieve 95%+ automation and 100% in-line testing, reducing attenuation, scrap, and time-to-market.

Q: How Do You Define The Scope Of FTTH Cable Production Line Technology?

A: FTTH cable production line technology covers the machinery, process controls, and materials for fiber-to-the-home networks. It includes optical fiber drawing and coating, SZ stranding, and ribbon formation. Extrusion of inner and outer jackets, armoring or taping modules, and automated take-up and drum handling are also part of it. In-line optical and mechanical testing, along with the software stack—PLCs, edge servers, and industrial IoT—are integral to the process.

Q: Why Does Production-Line Quality Matter For Broadband Network Infrastructure?

A: Production-line quality directly impacts attenuation, splice loss, mechanical robustness, and long-term reliability. High-precision manufacturing minimizes intrinsic and macrobending losses. It extends reach, lowers field interventions, and improves first-pass yields. For carriers and ISPs, this translates to fewer truck rolls, lower total cost of ownership, and higher service availability for high-speed internet, 5G backhaul, and symmetrical multi-gigabit home services.

Q: What Role Do PLCs And Smart Machinery Play In Industry 4.0 Production Lines?

A: Programmable logic controllers (PLCs) provide deterministic synchronization across SZ stranding, ribbon forming, and take-up units. They enable sub-0.01mm tension precision, closed-loop extrusion control, automated recipe changes, and safety interlocks. When combined with robotic arms and automated armoring modules, PLCs form the backbone of Industry 4.0 production. They drive repeatability and high throughput with minimal human intervention.

Q: How Are AGVs And Edge Computing Used On Modern Cable Production Floors?

A: Laser-navigated AGVs move heavy drums and material spools with high positioning accuracy. Industry examples show 1,200kg capacity and sub-5cm placement. Edge computing processes terabytes of telemetry locally, delivering low-latency analytics and real-time quality alerts. Together, AGVs and edge computing improve material flow, reduce manual handling risks, and enable rapid correction of process deviations.

Q: What Precision Engineering Improvements Reduce Optical Attenuation?

A: Improvements include ultra-low-loss (ULL) glass formulations and advanced UV-cured acrylate coatings. These coatings cut microbending losses. Smaller coated diameters (e.g., 160–180µm) enable denser cable designs. Tight control of drawing tension, coating cure profiles, and extrusion concentricity—monitored by laser micrometers and closed-loop controls—lowers intrinsic loss and fluctuation across production reels.

Q: How Do Central Strength Members And Mechanical Design Affect Cable Performance?

A: Mechanical designs incorporating fiber-reinforced plastic (FRP) rods or high-strength central members control elongation during installation. They resist crush and bending, protecting fiber glass from strain. Proper selection of strength elements and buffer constructions reduces installation-induced loss, improves long-term reliability, and supports aerial or duct deployments with demanding mechanical requirements.

Q: What Does “QC 4.0” Mean And How Is It Implemented?

A: QC 4.0 describes a fully instrumented, data-driven quality-control regime. It includes 100% in-line testing, AI-powered vision inspection, automated OTDR mapping, robotic bend tests, and environmental chambers integrated into the production workflow. Edge analytics, traceable test logs, and predictive models enable rapid root-cause analysis, minimize returns, and ensure compliance with ITU-T and operator specifications.

Q: How Is OTDR Testing Integrated Into Production And What Sensitivity Can It Achieve?

A: Automated OTDR stations are integrated inline or at take-up to perform full-length attenuation mapping. They use dual-wavelength sources (including 1550nm). Modern setups can detect variations down to 0.01 dB/km, map localized defects, and tie results to batch IDs for traceability. This enables manufacturers to flag and quarantine reels before shipment, improving field reliability.

Q: What Are Robotic Bend-Radius Simulators And Thermal Cycling Chambers Used For?

A: Robotic bend-radius simulators apply repeated controlled bends and record macrobend loss to verify compliance with ITU-T G.657 and customer specs. Thermal cycling chambers run jackets and assemblies through −60°C to +85°C cycles to validate dimensional stability, jacket adhesion, and splice performance under extremes. Automated test logs provide traceable evidence for operator and regulatory requirements.

Q: What Cable Design Innovations Are Most Relevant To FTTH Deployments?

A: Key innovations include bend-insensitive fiber (BIF) for tight routing in MDUs and indoor paths. Flat drop and high-fiber-count flat assemblies are used for aerial and direct-burial North American use cases. Microcables and air-blown systems are for duct-constrained environments. Pre-connectorized assemblies speed field activation and reduce termination errors.

Q: Why Is Bend-Insensitive Fiber Important For MDUs And Tight Routing?

A: Bend-insensitive fiber maintains low loss under tight radii and repeated handling. It is crucial in multi-dwelling units, plenum runs, and behind baseboards. ITU-T G.657-compliant fibers help prevent macrobending loss during installation and reduce service calls related to routing-induced degradation. They support denser routing with fewer installation constraints.

Q: How Do Flat Drop Cables And Microcables Differ In Deployment Benefits?

A: Flat drop cables offer flexible aerial and direct-burial deployment with compact profiles suited to service drops. Microcables (≤8mm) and microduct systems excel in congested ducts and enable incremental capacity growth via air-blown installation. Choice depends on regional deployment practice, span requirements, and operator preferences.

Q: What Advantages Do Pre-Connectorized Solutions Provide?

A: Factory-terminated, hardened pre-connectorized assemblies reduce field splicing, eliminate human termination variability, and speed up service activation. They improve first-pass yield. Products like hardened OptiTap-style connectors and vendor pre-terminated drops support rapid mass-deployment strategies and lower workforce training needs.

Q: How Are Energy Recovery And Cooling Innovations Improving Sustainability?

A: Regenerative drives on take-up reels and motor assemblies can capture braking energy, reducing net consumption by industry-reported amounts (example: up to ~32%). Chiller-less or adiabatic extrusion cooling reduces water use by up to 75%. These measures lower operational cost, reduce water consumption, and align production with corporate sustainability targets.

Q: Are Recyclable Jacket Materials And Waste Reduction Practical For Production?

A: Yes. Recyclable compounds such as specially formulated polypropylene-based jackets can meet mechanical and flame performance while improving end-of-life recycling. Precision extrusion and in-line inspection reduce scrap rates. Combined with material-efficient tooling and digital-twin optimization, manufacturers can materially lower waste and support circular-economy goals.

Q: What Role Do Digital Twins Play In Cable Manufacturing?

A: Digital twins create virtual replicas of production lines and cable designs to simulate process changes and validate material flow. They accelerate commissioning. Industry estimates show commissioning and prototyping time reduced significantly (case examples up to ~60%). Digital twins also support offline testing of recipe changes and faster roll-out of new product families.

Q: How Does AI Enable Predictive Maintenance And Quality Prediction?

A: Machine learning models trained on dozens of production parameters can forecast equipment faults hours in advance and predict quality drift. Predictive maintenance reduces unplanned downtime, improves OEE, and allows planned service windows. AI-driven quality models provide early alerts for deviations that would otherwise produce rejects or field failures.

Q: What Is The Significance Of Quantum And Distributed Sensing Integration In Cables?

A: Embedding distributed sensing capabilities—such as Brillouin-based strain sensing and distributed acoustic sensing (DAS)—adds network-level telemetry for structural health monitoring, intrusion detection, and environmental diagnostics. Integrating sensing into cable designs enables added-value services and improved operational visibility for carriers and critical infrastructure owners.

Q: How Do Production Lines Adapt To Regional Market Needs (North America, APAC, Europe)?

A: Lines are modular and reconfigurable to meet regional priorities. North America focuses on robust aerial and armored designs with higher breaking-strength requirements for pole deployments. APAC emphasizes high-density microcables and compact stranding for dense urban rollouts. Europe prioritizes halogen-free flame-retardant jackets and CPR fire-class compliance. Modular stranding towers, quick-change extrusion heads, and configurable armoring units enable fast changeovers.

Q: What Manufacturing Equipment Is Essential To Support Varied FTTH Product Families?

A: Essential equipment includes SZ stranding machines (dozens to hundreds of fibers with micron-level tension control), ribbonization lines, servo-driven extruders with laser micrometers, tape or armor-wrapping stations, automated take-up reels with regenerative drives, inline OTDR and AI vision inspection, AGV drum handling, and edge computing/PLC orchestration for Industry 4.0 integration.

Q: How Do Manufacturers Ensure Compliance With Standards Like ITU-T G.657 And Regional Safety Codes?

A: Compliance is ensured via precise material selection (bend-insensitive fiber types), controlled production recipes, automated in-line tests (OTDR, macrobend testers), and environmental qualification (thermal cycling, flame tests). Traceable test logs, batch IDs, and documented QC protocols align production outputs with ITU-T recommendations and regional regulations such as CPR classifications in Europe.

Q: What Benefits Can U.S. Manufacturers Expect From Equipment Suppliers Like Shanghai Weiye OFC Equipment?

A: Suppliers like Shanghai Weiye provide modular, Industry 4.0-ready production machinery—SZ stranding, ribbon lines, precision extrusion with closed-loop controls, AI inspection modules, and integrated OTDR testing. This enables U.S. contract manufacturers and in-house producers to scale FTTH output, maintain tight attenuation and mechanical tolerances, adopt sustainability options (energy recovery, closed-loop cooling), and shorten time-to-market for variants such as armored aerial, flat drop, microcable, and pre-connectorized assemblies.

Q: How Do In-Line AI Inspection Systems Detect Subtle Defects At Production Speed?

A: AI-powered machine vision inspects coating uniformity, surface defects, and microbends using high-resolution cameras and convolutional models trained on labeled defect libraries. Models correlate dozens of parameters—diameter variance, coating texture, micro-crack signatures—to predict deviations hours before they become out-of-spec reels. This enables automated rejection, parameter adjustment, and reduced downstream field failures.

Q: What Testing Sensitivity And Traceability Are Achievable For Attenuation And Mechanical Validation?

A: Modern production lines integrate automated OTDR systems capable of resolving 0.01 dB/km changes, robotic bend simulators for repeated macrobend stress testing, and thermal chambers for extreme environment validation. Test results are stored with batch and reel identifiers in edge or cloud databases, providing full traceability for operator acceptance, regulatory audits, and customer service diagnostics.

Q: How Do Production Innovations Translate Into Market Outcomes For Network Operators?

A: Innovations in manufacturing yield lower-loss fibers, denser cable designs, and factory-terminated assemblies that reduce installation time and errors. Operators benefit from higher service reliability, fewer truck rolls, lower lifecycle costs, and faster rollout of symmetrical multi-gigabit services. These outcomes support widespread FTTH adoption, 5G backhaul capacity, and scalable connectivity for smart cities and hyperscale data center interconnects.

Related: Lifecycle Costs of SZ Stranding Lines

Titanium Precision Parts for Deep-Sea Exploration

“Insight without implementation is hallucination.” – Thomas Edison. This insight cuts to the core of product development. A clever design stays an idea until it is transformed into a tangible, testable part.

UYEE Prototype connects this gap. We are a established provider of precision fabrication services. We focus on transforming the adaptable thermoplastic ABS into high-functioning components.

Titanium CCN Milling

ABS CNC Milling

Precision CNC Milling

Acrylonitrile Butadiene Styrene provides an outstanding balance of properties. It provides high impact resistance, solid strength, and dimensional stability. This makes it a preferred choice for structural applications across many fields.

Our sophisticated computer-controlled cutting process turns solid blocks into accurate, functional items. This approach bypasses the need for expensive injection molds. It is a economical path for low to medium-volume runs and rapid development cycles.

Industries from automotive to consumer electronics depend on these durable plastic parts. They are used for jigs, fixtures, and end-use products. The key is working with an experienced manufacturer.

UYEE Prototype brings together material science with manufacturing expertise. We guide clients through design for manufacturability and meeting tight tolerances. This partnership ensures your vision is brought to life with quality and efficiency.

Overview Of CNC Fabrication Of ABS Prototypes

The journey from digital design to physical part rests on selecting the right combination of material and manufacturing process. For countless engineers, the answer lies in a common thermoplastic and a precise, computer-controlled fabrication method.

This synergy produces durable, functional items ideal for testing and use. Understanding the material’s science and the process’s advantages is the first step.

What Is ABS Material? Understanding Acrylonitrile Butadiene Styrene

ABS stands for acrylonitrile butadiene styrene. It is a commonly used thermoplastic polymer. Its name reveals its three-monomer copolymer structure.

Acrylonitrile adds chemical resistance and thermal stability. Butadiene provides toughness and impact strength. Styrene brings rigidity and ease of processing.

This blend creates a material known for superb toughness and good dimensional stability. It maintains its shape under load, which is crucial for structural applications.

Titanium Precision Parts

“Material selection is the foundation of how your product performs.”

Engineering Fundamental

Key property metrics direct specification. Heat deflection temperature indicates how well a part performs under thermal stress. Rockwell hardness measures resistance to indentation.

Specialized grades, like ABS Flame Retardant, are available for added safety compliance. This variant meets specific industry standards.

Why Choose CNC Machining For ABS Prototypes?

Several methods exist for creating plastic parts. Computer-controlled cutting is especially valuable for functional models. It provides “true material behavior” since the item is milled from a solid block.

This preserves the full mechanical properties of the final production plastic. Other techniques, like vacuum casting, may use secondary materials that don’t match.

Process flexibility is a major advantage. Design iterations can happen rapidly without expensive tooling investment. It is perfect for low-volume runs and complex geometries.

The cost-effectiveness for small quantities is significant. High-quality surface finishes and precise details are achieved directly from the machine.

For functional testing, design validation, and presentation-quality models, this approach offers an optimal blend. It delivers fidelity, speed, and economic value.

At UYEE Prototype, our expertise in material science guides this selection. We ensure your components meet both performance and budgetary goals.

Advantages Of CNC Fabricated ABS Prototypes

Selecting the right method for creating plastic components rests on three fundamental pillars: economy, material performance, and precision. These advantages directly lead to reduced project risk and a smoother path from concept to validated product.

Cost-Effectiveness And Rapid Lead Times

The economic case for this fabrication method is compelling. It eliminates the high upfront cost of injection molds.

This makes it ideal for quantities from a single piece to over a hundred. The entry price point for initial models is very low.

Speed is equally critical. At UYEE Prototype, project lead times can start at just three days.

This rapid turnaround enables fast design iteration. It significantly shortens your overall time-to-market.

Superior Material Properties: Strength, Toughness, And Dimensional Stability

The chosen thermoplastic delivers remarkable performance. It offers high impact resistance and good tensile strength.

This inherent durability and rigidity often outperform other commodity plastics at a similar cost. Components can absorb shock without failing.

Dimensional stability is a critical property. It ensures parts maintain their precise shape and fit within assemblies.

This stability holds true across a range of environmental temperature conditions. It is essential for functional testing and end-use uses.

Material Property Benefit for Engineered Parts
Strong Impact Resistance Handles drops and abrupt loads well, making it ideal for housings and enclosures.
Good Tensile Strength & Stiffness Helps parts retain structural integrity during tension and bending loads.
Strong Dimensional Stability Preserves accurate geometry and fit, crucial for assemblies.

Precision And Tight Tolerances In Fabrication

Geometric accuracy is a cornerstone of our service. Standard machining accuracies are held to ±0.010 inches.

Tighter dimensional limits, such as ±0.002 inches, are readily achievable. For demands below ±0.002 inches, our experts conduct a manual review to ensure feasibility.

Smart design optimizes both expense and quality. Avoid specifying excessively tight limits unless absolutely necessary.

Grouping features on the same axis planes minimizes machine complexity. Keeping internal corner radii and tapped hole sizes consistent reduces tool changes.

UYEE Prototype offers components in natural beige, white, or black. For surface texture, you may choose the standard “As Machined” look or a uniform matte “Bead Blast” surface finish.

“Precise prototypes help validate precise production.”

UYEE Prototype Fabrication Principle

These advantages combine to deliver reliable, high-fidelity parts. They empower your product development team to reduce risk and confirm performance with confidence.

Uses And Industries For ABS Prototypes

From sleek consumer gadgets to rugged industrial equipment, specific thermoplastics prove their worth through versatile application. The theoretical benefits of precision-fabricated parts become concrete when they meet real-world demands.

This section explores major sectors where these components excel. Each industry leverages unique material properties to solve distinct challenges.

UYEE Prototype has extensive experience across these diverse fields. We help clients translate design intent into functional, reliable items.

Consumer Electronics: Housings And Enclosures

The consumer electronics sector demands a delicate balance. Parts must be lightweight yet durable, aesthetically pleasing, and precisely fitted.

This plastic offers an ideal combination of impact resistance and excellent surface finishability. It protects delicate internal circuitry while providing a sleek, user-friendly exterior.

Common applications include laptop cases, television bezels, and game controller bodies. These housings and enclosures require perfect fit for internal components.

Home appliance bodies also benefit from the material’s good strength and dimensional stability. UYEE’s fabrication ensures tight tolerances for seamless assembly.

This results in presentation-ready models that look and perform like final products. It allows for thorough user testing and design validation before high-volume production.

Automotive Components: Interior Trim And Functional Parts

In the automotive world, components face a harsh environment. They must withstand temperature fluctuations, UV exposure, and physical wear.

Interior trim pieces, like dashboard panels and pillar covers, are prime examples. The material provides a desirable feel, finish, and cost-effectiveness for these visible parts.

Its toughness and rigidity are crucial for functional items under the hood or on the exterior. Applications include grilles, spoilers, and specific bumper components.

“Proper material selection in the proper location shapes quality and safety in automotive engineering.”

Dimensional stability ensures these parts maintain their shape and fit across a wide temperature range. This property is non-negotiable for both safety and aesthetics in vehicle manufacturing.

From prototype to low-volume production, this approach allows for rapid iteration of complex geometries. It accelerates development cycles for both interior and exterior applications.

Industrial Manufacturing: Jigs, Fixtures, And Machine Housings

Industrial settings prioritize utility, durability, and cost-efficiency. Here, the focus shifts to custom tooling and equipment that streamline production.

Custom jigs, fixtures, and assembly aids are typical applications. These tools guide workers or machines during manufacturing, ensuring consistency and quality.

The material’s strength, machinability, and low cost make it perfect for these utilitarian roles. Protective housings for machinery and control panels are also common.

These enclosures and cable management parts shield sensitive electronics from dust, debris, and incidental impact. Rapid production of such custom components enables faster production line setup and modifications.

UYEE Prototype’s expertise ensures these industrial parts are robust and precisely made. They withstand the rigors of the factory floor, proving the material’s value from the design lab to operational deployment.

The versatility of this solution is clear. It supports innovation from initial concept through functional testing and into low-volume manufacturing.

By understanding sector-specific needs, UYEE delivers parts that perform as intended. This partnership turns ambitious designs into tangible, reliable components.

Why Partner With UYEE Prototype For Your ABS Needs

Your project’s outcome depends on a collaborator who understands both the science of materials and the art of fabrication. UYEE Prototype offers this dual expertise, guiding you to the optimal manufacturing process.

We provide deep knowledge of thermoplastics, including specialized grades for specific applications. Our team excels in precision fabrication, holding tight tolerances and machining complex geometries.

For functional testing and low-volume runs, computer-controlled cutting delivers true material properties in days. When appearance matters for small batches, vacuum casting offers a cost-effective alternative. High-volume production later benefits from injection molding.

We act as your consultative partner, offering design for manufacturability feedback to optimize cost and performance. Our rapid lead times and transparent pricing keep projects on schedule.

Value-added services like surface finishing and assembly deliver ready-to-use components. Submit your CAD files to our team for a professional review and quote. Let us transform your design into a tangible success.

Related: Explore Precision CNC Machining Solutions

The Bar Feeding in CNC Lathe Machining in Dallas

Can one tool improve part fit, reduce scrap, and accelerate time to market? Lowrance Machine is a Texas partner that provides production-ready results for plastic parts and finished products. Our team works from prototype to production, offering planning, tooling coordination, molding support, and guidance to keep cost and manufacturability on track.

Website About CNC Machine Shop in Dallas
We serve U.S. manufacturers and product teams who need repeatable quality, predictable timelines, and tight tolerances. Precision matters because it affects part fit, cosmetic finish, dimensional stability, and scrap rate.

Modern projects often call for flexible materials and processes like insert molding and overmolding to meet real-world performance needs. Lowrance Machine emphasizes clear communication, reliable outcomes, and customer-focused support across our facility and processes.

On this page you’ll find capabilities from prototype to production, design and engineering help, material options, specialized processes, QC practices, and lead-time expectations. Ready to move forward? Share your part files and requirements or request a quote from Lowrance Machine today.

Main Takeaways

  • Lowrance Machine provides turnkey tooling and molding support for dependable production.
  • Precision supports better fit, cleaner finish, and lower scrap rates.
  • Insert molding and overmolding address complex product requirements.
  • Clear communication and strict quality standards guide every project.
  • This page covers prototype to production, materials, processes, and lead times.

Precision Custom Mold Services In Dallas For Plastic Components And Products

Precision at Lowrance Machine means tighter tolerances, steady cycle-to-cycle output, and fewer assembly issues for parts and components.

We apply DFM principles—proper draft angles, uniform wall thickness, and smart gate placement—to reduce warpage, sink, and cosmetic blemishes. These mold design choices improve quality control and lower scrap rates.

Typical project inputs that drive success include part geometry, resin selection, expected volumes, packaging constraints, and end-use requirements. Lowrance Machine pairs these inputs with injection and injection molding processes for repeatable, high-volume plastics manufacturing.

Custom Molds in Dallas

  • Precision means tighter tolerances and more consistent output
  • Industries served: automotive and electronics manufacturing lines
  • Outcomes include better appearance, dependable function, and less rework
Focus Engineering Action Outcome
Draft angles Use taper for cleaner ejection Lower part damage
Part wall thickness Even sections Lower warpage risk
Gate location Optimize flow Better cosmetic finish

Choosing a precision-first approach reduces overall cost by cutting scrap, rework, and delays tied to unstable molding conditions. Share your requirements—part drawings, material preferences, and expected annual volumes—to start a practical conversation with Lowrance Machine.

Custom Mold Capabilities Built For Production, From Prototype To Full Runs

We build tooling roadmaps that take a part from validation to high-volume output with predictable results. Lowrance Machine guides product and engineering teams through prototype checks, bridge production, and full production runs so you can scale without reinventing strategy.

Our cavity strategy balances learning and efficiency. Single-cavity molds work for early validation while multi-cavity molds (up to 64 cavities) lower unit costs for steady production. Tooling choices — steel for long life or aluminum for fast turns — shape expected cycle counts and maintenance plans.

Typical planning separates tooling time (about 8–10 weeks) from production lead times (often 2–3 weeks once molds are ready). We match equipment to part envelope, clamp force, and shot size to keep process windows stable and efficiency high.

Phase Objective Typical Timeline
Prototype Testing and validation 2–4 weeks
Bridge stage Short runs, tooling tweaks Typically 2–12 weeks
Full-scale production Steady multi-cavity output Ongoing

Prepare CAD files, material targets, cosmetic notes, test plans, and volume forecasts to accelerate your project. Our team delivers clear communication, realistic timing, and tooling strategies that fit your production goals and product requirements.

Engineering And Mold Design Support That Lowers Risk And Improves Quality

Early design reviews at Lowrance Machine catch costly issues before tooling starts. Our team looks for common DFM risks: insufficient draft, uneven walls, unnecessary undercuts, and poor gate placement.

We recommend parting line and ejector pin layouts that protect visible surfaces and cut post-processing. These choices reduce cycles spent on rework and improve assembly fit.

Material selection ties directly to mold design. Resin shrink, flow, and temperature sensitivity shape gate size, runner balance, and cooling layout. We validate candidates with supplier data and test runs.

Injection planning (fill, pack, cool, eject) starts early. That reduces surprises at first articles and shortens ramp-up to production.

Risk Area Recommended Action Outcome
Undercut features Redesign or add lifters only when needed Lower tool cost, simpler maintenance
Wall thickness Balance sections and ribs Lower warpage with fewer sink marks
Gate and ejector layout Optimize location for flow and cosmetics Improved finish and easier assembly

How customers get best results: submit drawings, CTQ dimensions, performance targets, and any compliance or equipment requirements. Lowrance Machine acts as a solutions partner—guiding engineering choices that improve the finished product, not just the tooling.

Materials And Resin Options For Modern Plastics Manufacturing

Lowrance Machine starts by aligning resin families with your product goals, then fine-tunes molding and tool details.

We help teams pick materials that balance cost, manufacturability, and long-term performance for plastic products and components.

  • Polyethylene and polypropylene — versatile, economical choices for packaging and general parts.
  • ABS — durable material with attractive surface finish for consumer components.
  • Nylon — strength and durability for demanding functional components.
  • Polycarbonate & acrylic — clear, impact-resistant options where needed.
  • Polyester & styrene-based grades — durability or specialty properties.

We support virgin and recycled plastics when performance allows. Re-processed options reduce waste but need verification for consistent results.

Resin Type Relative Strength Typical Application
Polypropylene/Polyethylene Medium Packaging and housings
ABS resin Reliable Consumer components
Nylon/PC High Structural, high-heat parts
PMMA / Styrene-based grades Varies Optical, specialty

Resin choice affects gating, venting, cooling and how molds run. For regulated devices, we verify grades, supply documentation, and plan for cleanliness.

  1. Identify environment, loads, and appearance needs
  2. Confirm compliance and volume
  3. Match the material and molding method with Lowrance Machine

Specialized Molding Processes For Industry-Specific Needs

Process selection is where product goals meet manufacturing reality — and the right choice saves time and scrap.

Lowrance Machine helps match molding and forming options to industry requirements, balancing performance, cost, and production goals. We recommend processes that meet automotive, electronics, packaging, and device needs.

Overmolding applies a soft or durable layer over a substrate to add ergonomics, noise control, or grip. Insert molding places metal or preformed parts into the tool for a single-run assembly. Both require careful material compatibility checks for adhesion and durability.

  • Typical results include soft-grip handles, tactile buttons, and sealed multi-material assemblies used in consumer goods and devices.
  • Medical projects require tighter controls, stronger documentation, and often FDA-compliant or antimicrobial resin options.
Method Best Use Key Benefit
Overmolding Ergonomics, durability Adds soft-touch feel and vibration damping
Insert mold process Assemblies using inserts or fasteners One-step overmolded parts, fewer operations
Thermoforming Packaging and tray applications Reduced tooling cost and faster turnaround

Metal replacement molding uses engineered plastic to reduce weight, resist corrosion, and cut secondary machining. Choosing the right process early improves yield and reduces redesign late in the program.

Recommended next step: share end-use environment, industry constraints, and packaging expectations so Lowrance Machine can recommend the best-fit process and tooling approach.

Planable Quality Control, Equipment, And Lead Times

Well-documented checks and the right machines keep parts consistent from first shots to full runs. Quality control at Lowrance Machine starts with defined requirements, documented inspections, and routine review of critical dimensions and cosmetic standards.

First-article documentation confirms the tool, process settings, and part measurements before production continues. That report records sample measurements, machine parameters, and any adjustments needed to meet design requirements.

Equipment selection—clamp force, shot size, and process monitoring—supports precision and repeatability. Choosing the proper machine reduces variation for tighter-tolerance plastic parts and improves injection molding stability.

  1. Expect tooling to take around 8–10 weeks; production commonly begins 2–3 weeks after mold completion.
  2. Timelines may shift based on part complexity, cavity count, and resin choice.
  3. Provide packaging requirements early to protect cosmetic surfaces and ensure proper fit in trays or clamshells.
Equipment Capability Typical Range Reason It Matters
Clamping force 50–1,000 tons Supports part size and precision
Part weight and area Up to ~5 lbs / ~480 in² Determines machine and runner strategy
Component thickness Approximately up to 0.250 in Influences cooling and cycle timing

Stable processes cut downtime, scrap, and unplanned maintenance, which improves on-time delivery and overall efficiency. Communicate target delivery dates and packaging constraints early so Lowrance Machine can align a timeline and QC plan to your project requirements.

Request a confirmed schedule and inspection plan for your project to lock in tooling milestones and production delivery windows.

Final Thoughts

Select a manufacturer that converts engineering intent into repeatable production supported by clear timelines and data-driven quality checks.

Lowrance Machine provides focused services that prioritize predictable outcomes, practical guidance, and consistent quality for plastic parts and finished products. We align molds, materials, and process planning to reduce risk and speed time to delivery.

Good quality control and first-article documentation protect schedules and help customers scale with confidence. Specialized approaches — like insert molding, overmolding, or thermoforming for packaging — are available when the application requires a tailored solution.

Share your product goals, part files, and component requirements so Lowrance Machine can recommend the best path forward. Contact Lowrance Machine to request a quote and plan your next production run with confidence.

Related: CNC Machine Shop Dallas Explained: Quick Reference Guide